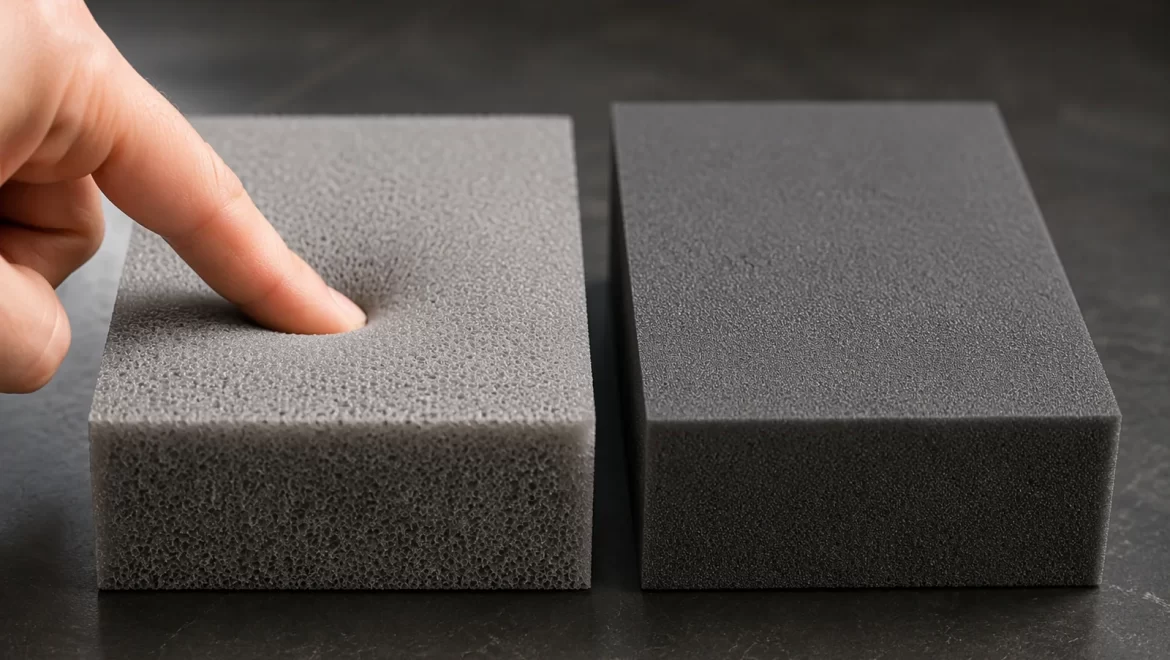
How Should Foam Density Be Chosen for Pet Bag Panels?
- Why Density Is the Number That Matters
- Reading a Foam Datasheet
- Density and Load Bearing
- Compression Set
- Indentation Hardness
- Foam Types in Bag Panels
- Interaction With Moulding and Pressing
- Density Across Panel Positions
- Weight and Portability
- Working With the Supplier
- Common Traps
- Testing and Verification
- Density and Durability Over Time
- Temperature and Climate
- Laminating Foam to Facings
- Fire and Safety Requirements
- Cost of Density
- Specifying Density: A Template
- Inspecting Incoming Foam
- Storage and Shelf Life
- Repair and Replacement
- Supplier Comparison
- Panel Assembly With Covers
- Density in Shaped and Moulded Panels
- Documentation and Traceability
- Recurring Specification Errors
- Measuring on the Finished Panel
- Limits of the Density Specification
- Matching Density to Animal Weight
- FAQ
Foam is bought by thickness and judged by feel, and both habits lead to the same failure: a panel that looks generous in the sample room and flattens under an animal within a season. Density is the property that decides whether a panel keeps its shape, and it is the one number that is rarely written down.
For a bag manufacturer, the density question is not "how soft should this feel" but "how much load must this panel carry, for how long, and at what temperature it will be pressed". This guide sets out how density, thickness, compression set and moulding interact, and how to write a foam specification that a supplier can meet and a buyer can verify.
Why Density Is the Number That Matters
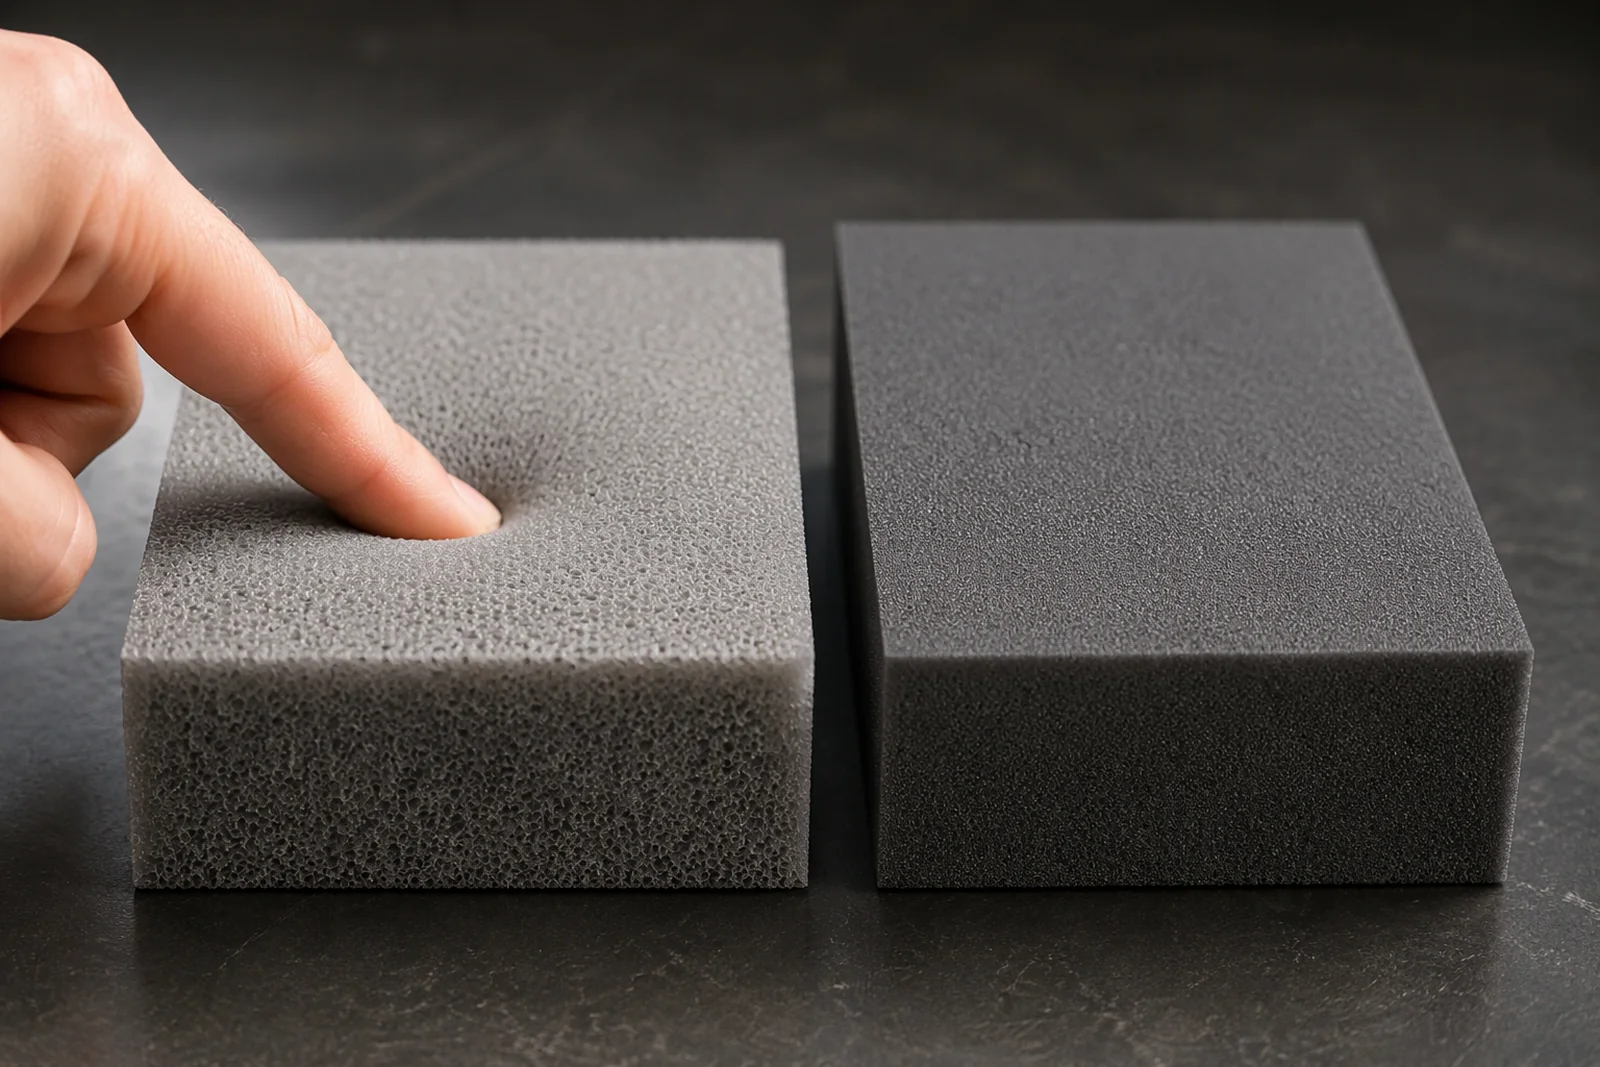
Density describes how much material sits in a given volume, and that single figure predicts most of what a panel will do in service.
Mass Per Volume
Density is measured as mass per unit volume and is normally quoted in kilograms per cubic metre. A higher figure means more polymer in the same space, which resists compression for longer.
What Density Is Not
Density is not hardness. Two foams of the same density can feel very different because of cell structure and formulation, so hardness and density must be specified separately.
The Commercial Consequence
A supplier that reduces density by a small margin saves material across every panel and changes the life of the bag. It is the most common silent substitution in soft-component supply.
Reading a Foam Datasheet
A datasheet carries the numbers that matter, and most of it can be ignored once four fields have been checked.
The Four Fields
Density, compression set, indentation hardness and tensile strength cover the behaviour that matters in a bag panel. Anything else is secondary for this application.
Test Conditions
Every figure is meaningless without its test condition. Density is straightforward; compression set and hardness depend on temperature, time and the amount of compression applied.
Grade Names
Names such as standard, high resilience and firm are marketing terms. They vary between suppliers and cannot be compared across them without the underlying numbers.
| Datasheet field | Why it matters in a bag | Typical spread |
|---|---|---|
| Density | Life under load | Narrow |
| Compression set | Recovery after packing | Wide |
| Indentation hardness | Feel and support | Wide |
| Tensile strength | Resistance to tearing | Moderate |
Density and Load Bearing
The relationship between density and support is direct but not linear, and thickness changes the conclusion.
Support at a Given Thickness
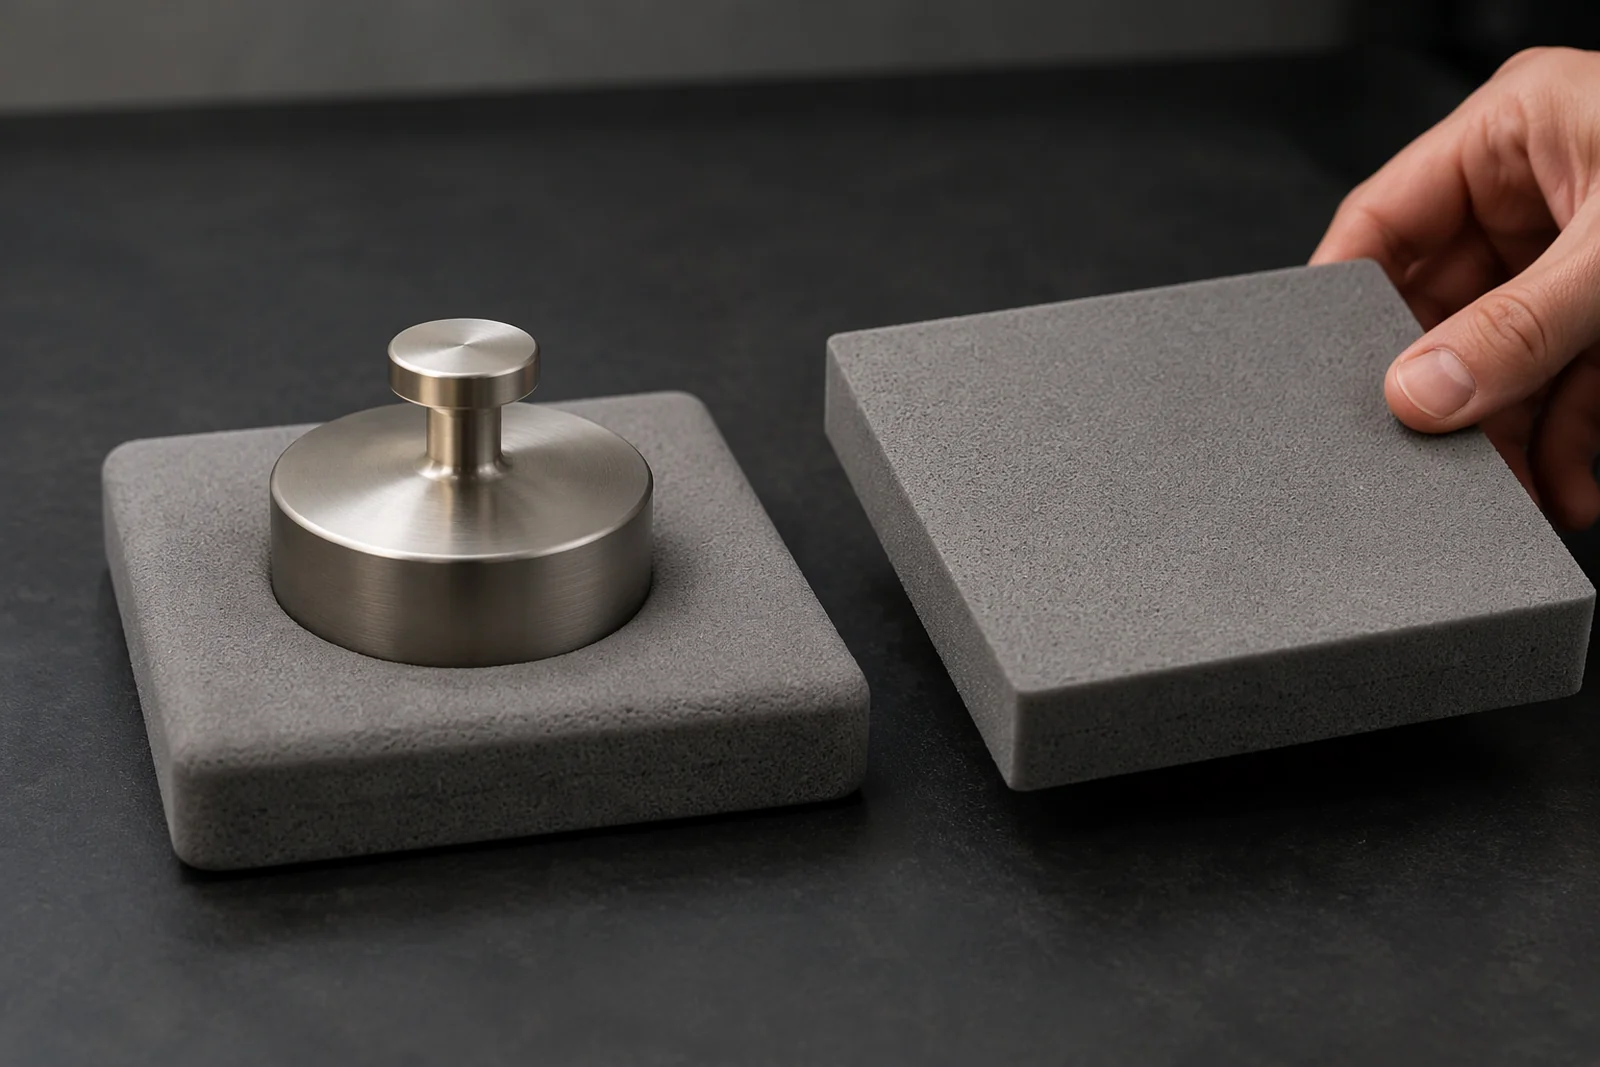
At a fixed thickness, a denser foam carries more load before it bottoms out. This is the simplest and most reliable rule in panel design.
The Thickness Effect
Thickness reduces the pressure felt at the surface for the same load. A thick low-density foam can feel supportive in the hand and still bottom out when the load is concentrated.
Bottoming Out
When a foam compresses to its solid height, support stops and the panel becomes a hard plate. The load at which that happens is the number a specification should control.
| Build | Density | Thickness | Load before bottoming |
|---|---|---|---|
| Soft and thick | Low | High | Low |
| Firm and thin | High | Low | Moderate |
| Firm and thick | High | High | High |
| Soft and thin | Low | Low | Very low |
Compression Set
Compression set is the property that separates a foam that survives a season from one that does not, and it is rarely quoted by suppliers unless asked.
What It Measures
A sample is compressed by a stated proportion, held at a stated temperature for a stated time, released and measured. The permanent loss of thickness is the set.
Why It Matters in a Bag
A carrier is stored folded and shipped compressed. A foam with poor set recovery arrives thin and stays thin, and the panel never reaches its nominal thickness.
Reading the Result
A low set figure means good recovery. A high one means the panel will lose height wherever it is packed under load, which is exactly where the base sits.
Indentation Hardness
Hardness describes how the surface resists a small loaded area, and it is what a buyer feels when pressing a panel with a thumb.
The Measurement
A disc is pressed into the foam and the force at a stated deflection is recorded. The result describes surface firmness rather than overall support.
Hardness Against Density
A high-density soft foam and a low-density firm foam can feel identical at the surface and behave completely differently under a standing animal. Both numbers are needed.
Choosing a Target
Firm enough to spread load, soft enough to avoid pressure points. Most panel programmes settle in a middle band and adjust thickness rather than hardness.
Foam Types in Bag Panels
Four foam families appear in pet bag panels, and each has a density range and a behaviour that suits different positions.
Polyethylene
Closed-cell polyethylene is the workhorse for base panels and structural inserts. It is available across a wide density range and takes no water.
Polyurethane
Flexible polyurethane is softer and more conformable, and open-cell grades absorb water. Closed-cell PU grades exist and cost more.
Ethylene Vinyl Acetate
EVA is light, resilient and easy to mould, and it is well suited to shaped panels and edges. Density and hardness vary widely between grades.
Recycled and Rebond
Rebond foam is made from shredded scrap and bonded, which gives high density and variable consistency. It suits structural filler where weight is acceptable.
| Family | Density range | Water | Typical use |
|---|---|---|---|
| Polyethylene | Wide | Closed | Base, inserts |
| Polyurethane | Wide | Open or closed | Comfort layers |
| EVA | Medium | Closed | Shaped panels |
| Rebond | High | Open | Filler, structure |
Interaction With Moulding and Pressing
Many panels are heat pressed or moulded into shape, and the pressing process changes the foam at the same time as it changes the panel.
Heat and Cell Structure
A thermoplastic foam softens under heat and the cells collapse if the pressure is high relative to density. A low-density foam loses thickness permanently at conditions a high-density one tolerates.
Pressing Reduces Thickness
Every press cycle reduces thickness slightly. The specification should state the thickness after pressing, not the thickness of the incoming sheet.
Laminated Assemblies
A foam laminated to fabric or board takes the press conditions of the whole stack. A foam that works alone can fail when pressed against a stiff facing.
Recovery After Moulding
A moulded panel should be measured after a settling period. Measuring immediately after the press gives a figure the customer will never see.
Density Across Panel Positions
One bag contains panels with different jobs, and specifying a single density everywhere wastes material in some places and under-supports others.
Base and Floor Panels
The floor carries the full weight on a small area. It needs the highest density in the bag and enough thickness to avoid bottoming out.
Wall and Side Panels
Walls carry leaning contact and need shape retention more than load capacity. A medium density holds the wall flat under its own weight.
Lid and Top Panels
The lid holds shape and takes little load. A lower density with good recovery is adequate and keeps the bag light.
Edge and Handle Areas
Where the panel meets a handle or strap, the foam must resist local compression. Dense inserts at those points are cheaper than raising density everywhere.
Weight and Portability
Density is weight, and weight at the base of a carried bag is felt directly by the customer.
The Weight Arithmetic
Weight rises linearly with density at a fixed volume. Doubling density doubles the panel weight, which is a real cost in a bag designed to be carried.
Stiffness Per Gram
Stiffness rises faster than weight when thickness is increased instead of density. Thicker light foam is often the better engineering choice.
Where Weight Is Acceptable
At the base, some weight is useful for stability. At the top and sides, weight adds fatigue without adding function.
| Change | Weight | Support | Best for |
|---|---|---|---|
| Raise density | Up sharply | Up | Base |
| Raise thickness | Up moderately | Up | Walls |
| Raise both | Up sharply | Up | Large bags |
| Lower both | Down | Down | Lid, light bags |
Working With the Supplier
Foam is supplied to a density tolerance, and the tolerance is where substitution happens.
Specify a Range
State density as a nominal figure with a permitted tolerance. Without a tolerance the supplier may deliver at the bottom of the range and remain compliant.
Ask for the Batch Figure
Request the measured density of the delivered batch, not the datasheet figure. The batch number is the one that applies to the goods in hand.
Verify by Weight and Volume
Density can be checked with a scale and a measured cut sample. A simple weight and volume check catches most substitutions without laboratory equipment.
Certificate and Sample
Keep a certificate for the batch and a retained sample of the foam. Together they settle a dispute in a way that a conversation cannot.
Common Traps
Six traps account for most density problems in bag panels, and every one of them is preventable at the specification stage.
Buying by Thickness Alone
Thickness is visible and density is not. A panel specified only by thickness invites a lighter foam at the same thickness.
Comparing Grade Names
Two suppliers use the same grade name for different foams. Comparison requires the numbers, not the words.
Ignoring Compression Set
A foam with good density and poor set recovery still arrives flat after a season in a carton. Set belongs in the specification.
Measuring Before Recovery
Measuring a moulded panel immediately after pressing understates the thickness that reaches the customer.
Single Density Everywhere
One density across all panels either wastes material or under-supports the floor. Position-based grading is the cheaper answer.
No Retained Sample
Without a physical sample the agreed foam cannot be compared to the delivered foam. The sample is the specification in practice.
Testing and Verification
Verification of foam density is quick, and it fits inside an incoming inspection routine without special equipment.
The Cut Sample Method
Cut a known volume, weigh it and divide. The result is density in the units on the specification and it takes minutes.
Compression Set Check
Compress a sample by a stated proportion for a stated time, release and measure. The recovery figure catches foams that pass a density check and fail in use.
Hardness by Hand and by Instrument
A durometer or a simple indentation rig gives a repeatable figure. Hand feel is useful for a first look and useless for a record.
| Check | Equipment | Time | Detects |
|---|---|---|---|
| Density | Scale and rule | Minutes | Substitution |
| Compression set | Clamp and oven | Hours | Poor recovery |
| Hardness | Durometer | Minutes | Wrong grade |
| Thickness | Gauge | Minutes | Press loss |
Density and Durability Over Time
A panel is specified for the day it is made, and it is judged after a year of use in a bag that is folded, stored and carried.
Fatigue Under Cycling
Repeated loading softens foam progressively, and the rate depends on density and on how close the load sits to the bottoming point. A panel loaded near its limit fatigues fastest.
Set Accumulation
Each compression leaves a small permanent loss. A foam with a modest set figure accumulates less over hundreds of cycles, which is where the customer's judgement is formed.
Visible Consequences
The panel thins, the cover loosens, the floor no longer sits flat and the animal's weight reaches the base board. All four are density outcomes rather than cover outcomes.
Temperature and Climate
Foam softens when warm and stiffens when cold, and a bag crosses both conditions between a factory and a home.
Heat Softening
Near its softening range a thermoplastic foam loses support quickly. A panel that is adequate at room temperature can bottom out in a hot vehicle.
Cold Stiffness
In cold conditions foam becomes firm and less conformable. A dense foam that feels supportive in summer can feel hard in winter.
Shipping and Storage Extremes
A container in a hot port reaches temperatures well above ambient. Foam that is compressed in that container takes a set that never fully recovers.
Laminating Foam to Facings
Foam is rarely used bare, and the lamination step changes both the thickness and the density behaviour of the assembly.
Adhesive Weight
Adhesive adds mass and can add stiffness. The panel density quoted to a customer should describe the foam, with the assembly weight stated separately.
Flame Lamination
Flame lamination bonds foam to fabric without adhesive and slightly compresses the surface cells. The compressed layer is denser and thinner than the core.
Press Conditions
Temperature and pressure during lamination determine how much thickness is lost. The finished thickness is the number to specify.
| Lamination | Thickness loss | Surface effect |
|---|---|---|
| Adhesive | Minimal | Slight stiffening |
| Flame | Moderate | Denser skin |
| Hot melt sheet | Low | Even bond |
| None | None | Bare foam |
Fire and Safety Requirements
Foam is a combustible material inside a textile product, and the requirement differs by market and by channel.
What Applies
Requirements depend on the destination market and on how the product is classified. The applicable standard belongs in the specification, named explicitly.
Documentation
A supplier declaration and a test report for the foam grade are the two documents a buyer should hold. Both should name the grade, not the family.
Design as the First Control
Foam enclosed behind a cover, away from ignition sources and sized to avoid large exposed surfaces, reduces risk before any chemistry is considered.
Cost of Density
Density is the largest single driver of foam cost, and the cost curve is steeper than most buyers expect at the top of the range.
Material Share
Foam is priced largely by mass, so density sets material cost almost directly. A step up in density is a step up in cost per panel.
The Cheaper Route
Raising thickness at constant density adds cost more slowly than raising density, and it often delivers the same support. Thickness is the first lever.
Position-Based Grading
Dense foam only where load is concentrated, and lighter foam elsewhere, delivers the same performance as a uniform upgrade at a lower total cost.
| Route | Cost | Support | Weight |
|---|---|---|---|
| Uniform density rise | High | High | High |
| Thickness rise | Moderate | High | Moderate |
| Local dense inserts | Low | Targeted | Low |
| Lower density everywhere | Low | Low | Low |
Specifying Density: A Template
A foam requirement fits in six lines on a purchase order, and each line closes a specific route to substitution.
The Six Lines
Family and grade, density with tolerance, thickness after forming, hardness range, compression set limit and the test conditions. Together they define the material without ambiguity.
What to Leave Out
Colour names, supplier-specific codes and descriptions of feel. None of them can be verified and all of them invite interpretation.
Attaching the Sample
Reference a retained sample by a code that appears on the drawing. The physical sample and the written figure then support each other.
| Line | Example form | Verification |
|---|---|---|
| Family | Closed-cell polyethylene | Certificate |
| Density | Nominal plus tolerance | Weight and volume |
| Thickness | After pressing | Gauge |
| Hardness | Range at stated deflection | Durometer |
| Set | Maximum at stated conditions | Clamp test |
Inspecting Incoming Foam
Incoming inspection is the last point where a substitution can be caught cheaply, and it needs a routine rather than a procedure.
Frequency
Check the first delivery of a batch and then at intervals. Density substitutions usually appear as a new batch rather than as a gradual drift.
What to Sample
Cut from the middle and from the edge of the sheet. Skin effects at the edge give a different figure from the core.
Recording
Record the measured figure against the batch number. A trend across batches shows a supplier drifting before a customer does.
Storage and Shelf Life
Foam changes while it waits, and a panel made from aged foam is a different panel from one made from fresh stock.
Compression in Storage
Sheets stacked high compress the bottom layers. Stored flat and uncompressed, foam keeps its thickness; stacked and bound, it takes a set.
Light and Heat
Prolonged exposure to light and heat ages the surface. Foam stored near a roof or a window can be unusable at the surface while the core is sound.
Age Before Use
Old foam may already have taken a permanent set. Recording the delivery date and using stock in order costs nothing and prevents that.
Humidity in Storage
Closed-cell foam ignores humidity and open-cell foam does not. A sheet of open-cell foam stored in a humid warehouse takes up water, gains mass and loses the support it was specified for. Weighing a stored sheet against its delivery figure shows whether that has happened, and it explains a batch that measures heavy and feels soft at the same time.
Repair and Replacement
A foam panel is not normally repairable, and the design should accept that rather than pretend otherwise.
When Foam Fails
Thinning, permanent set and crumbling are not recoverable. The panel is replaced, not restored, once the foam has collapsed.
Access for Replacement
A panel held in a sleeve or a pocket can be replaced. A panel bonded to the shell cannot, and that decision belongs in the design.
Selling the Insert
A replaceable foam insert extends the life of the shell and is a low-cost accessory with a clear purpose.
Supplier Comparison
Comparing foam suppliers means comparing numbers under the same conditions, and the differences are usually larger than expected.
Same Density, Different Feel
Two foams at the same density can differ in hardness by a wide margin. The comparison has to include hardness or it describes only mass.
Same Grade, Different Set
Compression set varies more between suppliers than density does, and it is the figure most often missing from a quotation.
The Comparison Set
Density, hardness, set and thickness after pressing, all measured on samples from both suppliers under the same conditions.
| Compared item | Spread seen | Effect in use |
|---|---|---|
| Density | Narrow | Life under load |
| Hardness | Wide | Feel and pressure |
| Compression set | Wide | Recovery after storage |
| Thickness after press | Moderate | Final panel height |
Panel Assembly With Covers
A foam panel is only as good as the cover that holds it, and the assembly can undo a correct density choice.
Cover Fit and Compression
A cover cut tight compresses the foam before it is used. The panel then starts life already thinner than specified and fatigues faster.
Quilting Effects
Quilting compresses foam along the stitch lines and creates dense bands. Those bands change how the panel carries load across its surface.
Edge Behaviour
At a bound edge the foam is compressed into the binding. On a light foam the compressed edge becomes the hardest part of the panel.
| Assembly | Effect on foam | Mitigation |
|---|---|---|
| Tight cover | Pre-compressed | Allow cavity plus small fit |
| Quilting | Local dense bands | Space stitch lines |
| Bound edge | Compressed rim | Match foam to binding |
| Bonded facing | Denser skin | Specify final thickness |
Density in Shaped and Moulded Panels
Shaped panels concentrate the density question, because moulding redistributes material rather than preserving it.
Wall Thinning
A moulded shape draws material and thins where the draw is deepest. The thin area is also the area most likely to be loaded.
Corner Density
Corners draw less and stay denser, which is usually helpful. Where a corner should be soft, the mould has to be designed for it.
Measuring the Finished Part
Measure density and thickness at several points on the finished part, not on the sheet. The sheet figure describes the input, not the product.
Documentation and Traceability
Density is a number that has to travel with the goods, and a panel without its figure cannot be defended or reordered.
On the Drawing
The density, its tolerance and the test method belong on the panel drawing. A separate foam specification that is not referenced will be lost.
On the Batch Record
The batch record should carry the measured figure and the supplier lot. Together they connect a finished panel to the foam delivered.
For the Customer
Where a buyer requests material information, the density and family answer most of the question without disclosing the full formulation.
Recurring Specification Errors
The density mistakes that recur in production are few, and each has a simple control.
Quoting the Datasheet
The datasheet describes a nominal product. The batch in hand is the material that will be built into the bag.
Confusing Density With Firmness
A buyer who asks for a firmer feel may be answered with a denser foam when a harder one at the same density would be correct.
Ignoring Press Loss
Thickness lost in moulding is thickness the customer never receives. Specifying incoming thickness instead of finished thickness hides the loss.
One Density for the Whole Bag
Uniform density either overbuilds the walls or underbuilds the floor. Position-based grading resolves both.
No Tolerance Stated
Without a tolerance the supplier can deliver at the bottom of the range and be fully compliant.
Measuring Too Early
A moulded panel measured immediately after pressing reads thin. A settling period before measurement gives the figure the customer sees.
Measuring on the Finished Panel
A density figure taken from the sheet describes an input. What reaches the customer is the finished panel, and it has to be measured in place.
Sample Points
Measure at the centre, near the edge and at a corner of the finished panel. The three points show how moulding and assembly have redistributed the material.
Thickness Under Load
Measure the panel under a load close to the intended animal. An unloaded measurement describes a panel that no animal will ever stand on.
Recording the Assembly
Record the cover, the facing and the adhesive with the panel figure. The same foam inside a different cover behaves differently, and the record should show which combination was measured.
| Point | What it reveals | Typical finding |
|---|---|---|
| Centre | Core density | Closest to sheet |
| Edge | Press and binding loss | Thinner, denser |
| Corner | Mould draw | Variable |
Limits of the Density Specification
Density predicts a great deal and it does not predict everything, and stating the limits keeps a specification honest.
What Density Cannot Predict
Cell structure, formulation and the effect of heat. Two foams at the same density can fail differently under the same load.
What It Should Not Promise
A specific number of years of service, a load rating for an animal of a given weight, or a performance guarantee at any temperature.
Where the Real Control Sits
Density plus hardness plus compression set, measured on the finished panel, is the combination that can be defended. Density alone is a starting point.
Matching Density to Animal Weight
A carrier is made for a weight range, and the panel density should follow that range rather than the style of the bag.
Small Animals
A light animal loads a small area lightly, so a medium-density foam at modest thickness carries it without bottoming out. Dense foam here adds weight for nothing.
Medium and Large Animals
A heavier animal loads the floor near its limit. Density and thickness must rise together, or the panel will bottom out at the first standing turn.
Weight Bands in the Specification
State the intended animal weight band per size on the drawing. Density then follows from a stated requirement rather than from a preference.
| Size band | Density route | Thickness route |
|---|---|---|
| Small | Medium | Moderate |
| Medium | Medium to high | Moderate to high |
| Large | High | High |
| Extra large | High plus inserts | High |
FAQ
Should the density be verified on the panel rather than the sheet?
A: On the panel. Moulding, lamination and the cover all change the thickness and the effective density, so the finished part is the only figure that describes the product.
Is higher foam density always better?
A: No. Density adds support and weight together. Above the point the panel needs, extra density costs money and makes the bag heavier without improving life.
How is foam density measured?
A: Cut a known volume, weigh it and divide. The figure is mass per unit volume, and it can be checked at goods-in with a scale and a rule.
What is the difference between density and hardness?
A: Density is how much material is in the volume; hardness is how the surface resists a small loaded area. Two foams at the same density can feel very different.
Why does a foam panel arrive thinner than specified?
A: Because thickness was specified on the incoming sheet rather than after pressing, lamination or storage under load. The finished figure is the one to write down.
What is compression set and why does it matter?
A: It is the permanent loss of thickness after compression at a stated temperature and time. A carrier is stored folded, so poor set recovery means a panel that stays thin.
Which foam suits a washable panel?
A: A closed-cell foam, typically polyethylene or a closed-cell PU grade. Open-cell foam holds water and odour and cannot support a wash claim.
Should density be the same across the whole bag?
A: No. The floor needs the highest density, the walls and lid less. Position-based grading delivers the same support for less weight and cost.
What tolerance should be allowed on density?
A: A stated nominal with a permitted range, written on the drawing. Without a tolerance a supplier can deliver at the bottom of the range and still comply.
Can density be verified without a laboratory?
A: Yes. A cut sample, a scale and a rule give a usable figure, and a clamp test with an oven gives a compression set result.
Does moulding change the density?
A: It changes the finished part. Moulding thins the material where the draw is deepest, so the density and thickness of the part differ from the sheet.
How does flame lamination affect the panel?
A: It compresses the surface cells and creates a denser skin while reducing thickness slightly. Measure the assembly after lamination rather than assuming the sheet figure.
How should a foam be stored before use?
A: Flat, uncompressed, away from heat and light, and used in delivery order. Foam stacked and bound takes a set that it will not fully recover.
What belongs on the panel drawing?
A: Family, density with tolerance, finished thickness, hardness range and compression set limit, each with its test conditions and a retained sample code.
Is a denser foam worth the cost at the base?
A: Usually yes, because the base is the panel that cannot be replaced and the one that carries the full weight. Elsewhere the cost is harder to justify.
What can a density figure not guarantee?
A: Years of service, a load rating for a specific animal, or performance at any temperature. Density, hardness and set measured on the finished part is the defensible combination.
Ready to stop guessing at foam by feel? Put density with a tolerance, finished thickness and a compression set limit on the panel drawing, grade density by position, and check the delivered batch by weight and volume before it reaches the cutting table.