Working with a Bag Factory Remotely: How to Avoid Errors
- Why Remote Collaboration Fails
- The Specification Handoff
- Sample Feedback That Produces the Right Change
- Communication Cadence
- Documentation and a Single Source of Truth
- Inspecting a Factory Remotely
- The Classic Errors and How to Prevent Them
- Managing Quality Without Being There
- When Travelling Is Worth It
- Working Through Agents and Trading Companies
- Language, Translation and Visual Communication
- Costing and Commercial Clarity at a Distance
- Building Trust Without Meeting
- A Remote Collaboration Playbook by Stage
- Tools That Reduce Remote Friction
- Onboarding a New Factory Remotely
- FAQ
Most brands that source leather bags do it from a different country than the factory. The relationship runs on specifications, photographs, sample shipments and messages rather than on walking the floor together. That arrangement works, but it fails in predictable ways.
Errors in remote collaboration are rarely caused by bad faith. They come from information that was never transmitted, assumptions that were never tested, feedback that arrived in a form the factory could not act on, and decisions that were made verbally and never written down. Each of these is manageable with discipline rather than travel.
This guide covers where remote collaboration breaks down, how to hand off a specification properly, how to give sample feedback that produces the right change on the first attempt, how to set a communication cadence that survives time zones, how to keep one authoritative version of the truth, how to inspect a factory remotely, and when flying there is genuinely the cheaper option.
Why Remote Collaboration Fails
The failure modes cluster into a few categories, and each has a different remedy.
Language and Terminology Gaps
Technical vocabulary does not translate cleanly. Terms such as "edge finishing", "structure", "soft touch" or "premium feel" mean different things to different listeners, and a translated specification can lose the distinction between a requirement and a preference.
The practical response is to reduce reliance on adjectives. Measurements, reference photographs and physical samples carry meaning that language does not.
Time Zone Arithmetic
A twelve-hour offset means every question costs a day, and a project with twenty open questions can drift for weeks. Messages sent at the end of one working day arrive during the other side's night and are answered a full cycle later.
The remedy is batching: consolidate questions into a single structured list so one cycle answers all of them, rather than exchanging twenty messages over twenty days.
Tacit Knowledge That Does Not Travel
Factory staff know things that were never written down: which leather lots run consistent, which machine needs adjusting on thick panels, which operation tends to drift. On site, that knowledge is absorbed by observation. Remotely, it has to be surfaced deliberately through questions.
Ambiguity About Authority
When several people on each side communicate, feedback can arrive from multiple directions with differing instructions. The factory resolves the conflict by choosing one interpretation, and the brand discovers the error at the sample review.
Designating one point of contact on each side, with final authority on approvals, removes most of this class of error.
| Failure mode | Typical symptom | Structural remedy |
|---|---|---|
| Vocabulary gaps | Sample differs from intent | Measurements and reference photos |
| Time zone lag | Weeks lost to question cycles | Batched question lists |
| Tacit knowledge | Repeated avoidable defects | Structured questioning |
| Split authority | Conflicting instructions | Single contacts with authority |
| Verbal changes | Production differs from approval | Written change records |
The Specification Handoff
The specification is the foundation of a remote relationship. If it is incomplete, every later stage inherits the gap.
Building a Complete Tech Pack
A tech pack should let a factory build the product without asking what was meant. That means dimensions with tolerances, construction notes, material specification down to the lining and interlining, hardware with finishes and sizes, stitch specification, edge treatment and labeling.
Completeness matters more than length. A short pack covering every element that changes an outcome outperforms a long pack with gaps.
Visual References
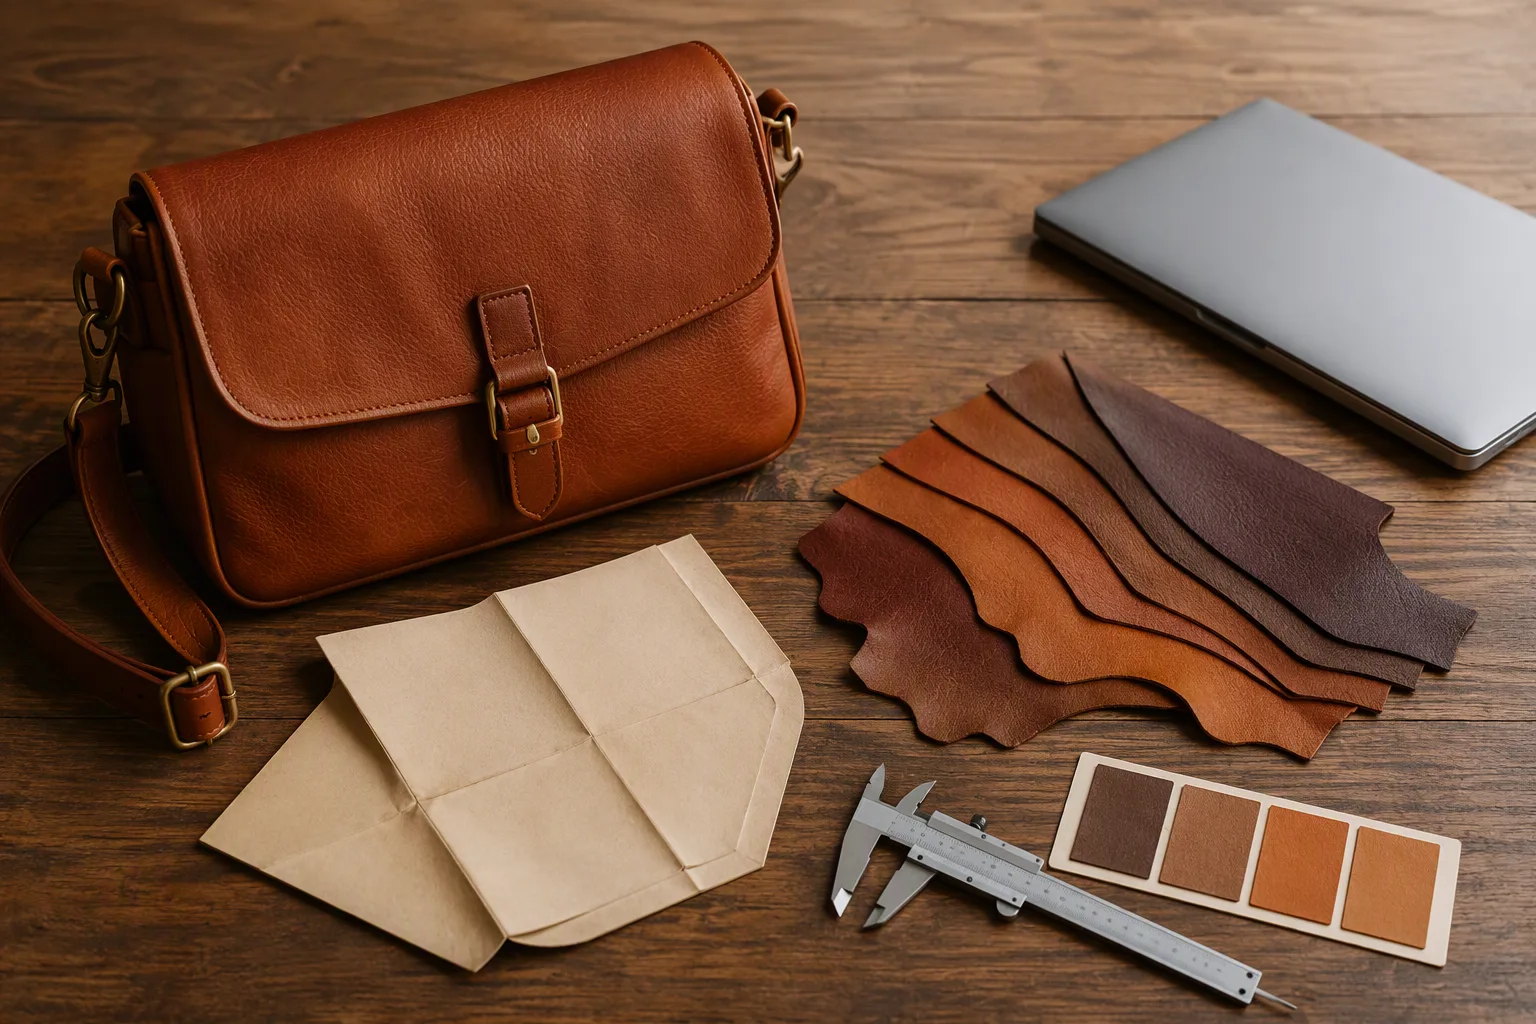
Photographs and physical references do more work than paragraphs. Include reference photographs of the intended construction, an approved physical sample where one exists, a color swatch with a reference code, and hardware samples or photographs with finish names.
Where a feature is hard to describe, mark up a photograph. An annotated image removes ambiguity that a written description cannot reach.
The Clarification Round
Before production, ask the factory to return a written summary of what they understand the product to be, including any points they consider unclear. This costs one cycle and prevents the most expensive category of error: a well-executed product that is not the product the brand intended.
What to Include in the Handoff
| Element | Purpose | Common omission |
|---|---|---|
| Dimensioned drawings | Defines geometry | Tolerances |
| Construction notes | Defines method | Edge and seam treatment |
| Material specification | Defines inputs | Lining and reinforcement |
| Hardware schedule | Defines components | Finish and size |
| Color references | Defines appearance | Reference codes |
| Stitch specification | Defines appearance and strength | Stitch density |
| Labeling requirements | Defines compliance | Placement and content |
| Reference sample | Defines the standard | Not sent for early rounds |
Sample Feedback That Produces the Right Change
Feedback quality determines how many rounds a development takes. Poor feedback does not fail immediately; it produces a sample that is different in the wrong way and a round that must be repeated.
Structure Every Comment
Number each comment, reference it to a photograph or measurement, state what is wrong, state what is required, and indicate priority. A comment that only describes a feeling invites interpretation.
Separate what must change from what could change. Mixing them equally produces either an over-engineered sample or an ignored requirement.
Photographs and Measurements
A photograph with a marker indicating the location, plus a measurement where a dimension is involved, gives the factory something actionable. Written descriptions alone often point at the wrong place.
For color and finish, compare against the approved swatch in the same lighting rather than describing tone in words.
One Round, One Version
Stacking changes across multiple rounds makes it impossible to attribute a difference to a specific instruction, and it lengthens development. Each round should carry a defined set of changes against a defined reference.
Feedback Template Fields
| Field | Content | Why it matters |
|---|---|---|
| Comment number | Sequential identifier | Traceability |
| Location | Photograph with marker | Prevents misreading |
| Observation | What was found | Shared understanding |
| Requirement | What is required | Actionable instruction |
| Priority | Must change or optional | Guides effort |
| Reference | Approved sample or spec | Removes ambiguity |
| Status | Open or closed | Tracks closure |
Communication Cadence
Remote projects fail slowly through silence. A predictable rhythm keeps both sides aligned without requiring constant contact.
A Regular Review Slot
A weekly or twice-weekly call at a fixed time, with a written agenda sent in advance, lets both sides prepare. Calls without an agenda become status updates that consume time without resolving decisions.
Between calls, a single written update from the factory covering progress, blockers and decisions needed keeps the project visible without requiring daily messages.
Channel Discipline
Use one channel for decisions and one for quick coordination, and never approve something in the informal channel. A decision that exists only in a chat thread is not a decision the factory can audit later.
Email or a shared document remains the record for approvals, changes and commitments, because it can be searched and forwarded.
Time Zone Working
Rotate meeting times so the inconvenience is shared rather than falling always on one side. Where a call is impractical, a written question list plus a short recorded video walkthrough covers most of what a call would achieve.
Set an explicit response expectation: for example, questions received by a cut-off time are answered the following working day. Without an expectation, response times drift and the project loses its rhythm.
| Cadence element | Frequency | Purpose |
|---|---|---|
| Project call | Weekly | Decisions and blockers |
| Written progress note | Twice weekly | Visibility between calls |
| Question list | As needed, batched | Reduce cycle count |
| Approval record | Per milestone | Traceable authority |
| Escalation channel | Defined in advance | Fast resolution |
Documentation and a Single Source of Truth
In remote work, an unrecorded decision is not a decision. Documentation is what allows two organizations in different countries to act as one team.
Version Control and Naming
Every specification, photograph set and comment list should carry a version identifier and a date. Superseded versions should be marked as such rather than deleted, so the history of a decision remains traceable.
File names should indicate product, element and version, so a factory can identify the current document without asking.
The Change Log
Each change should be recorded with what changed, why, who approved it and when it takes effect. The change log is what prevents a future batch from being built to a retired specification.
Where a change affects cost, tooling or lead time, the factory should confirm the impact in writing before the change is implemented.
Approval Authority
State who can approve what: materials, construction, measurements, labeling. When an approval arrives from someone without authority, the factory has no way to know, and the error appears later in production.
Documents That Should Exist
| Document | Owner | Update trigger |
|---|---|---|
| Technical specification | Brand | Design change |
| Approved sample record | Both | Sample approval |
| Change log | Brand | Any approved change |
| Sample feedback log | Brand | Each review round |
| Inspection criteria | Both | Quality standard change |
| Labeling specification | Brand | Market requirement change |
Inspecting a Factory Remotely
Distance does not remove the need to verify, but it changes how verification is done.
Remote Walkthroughs
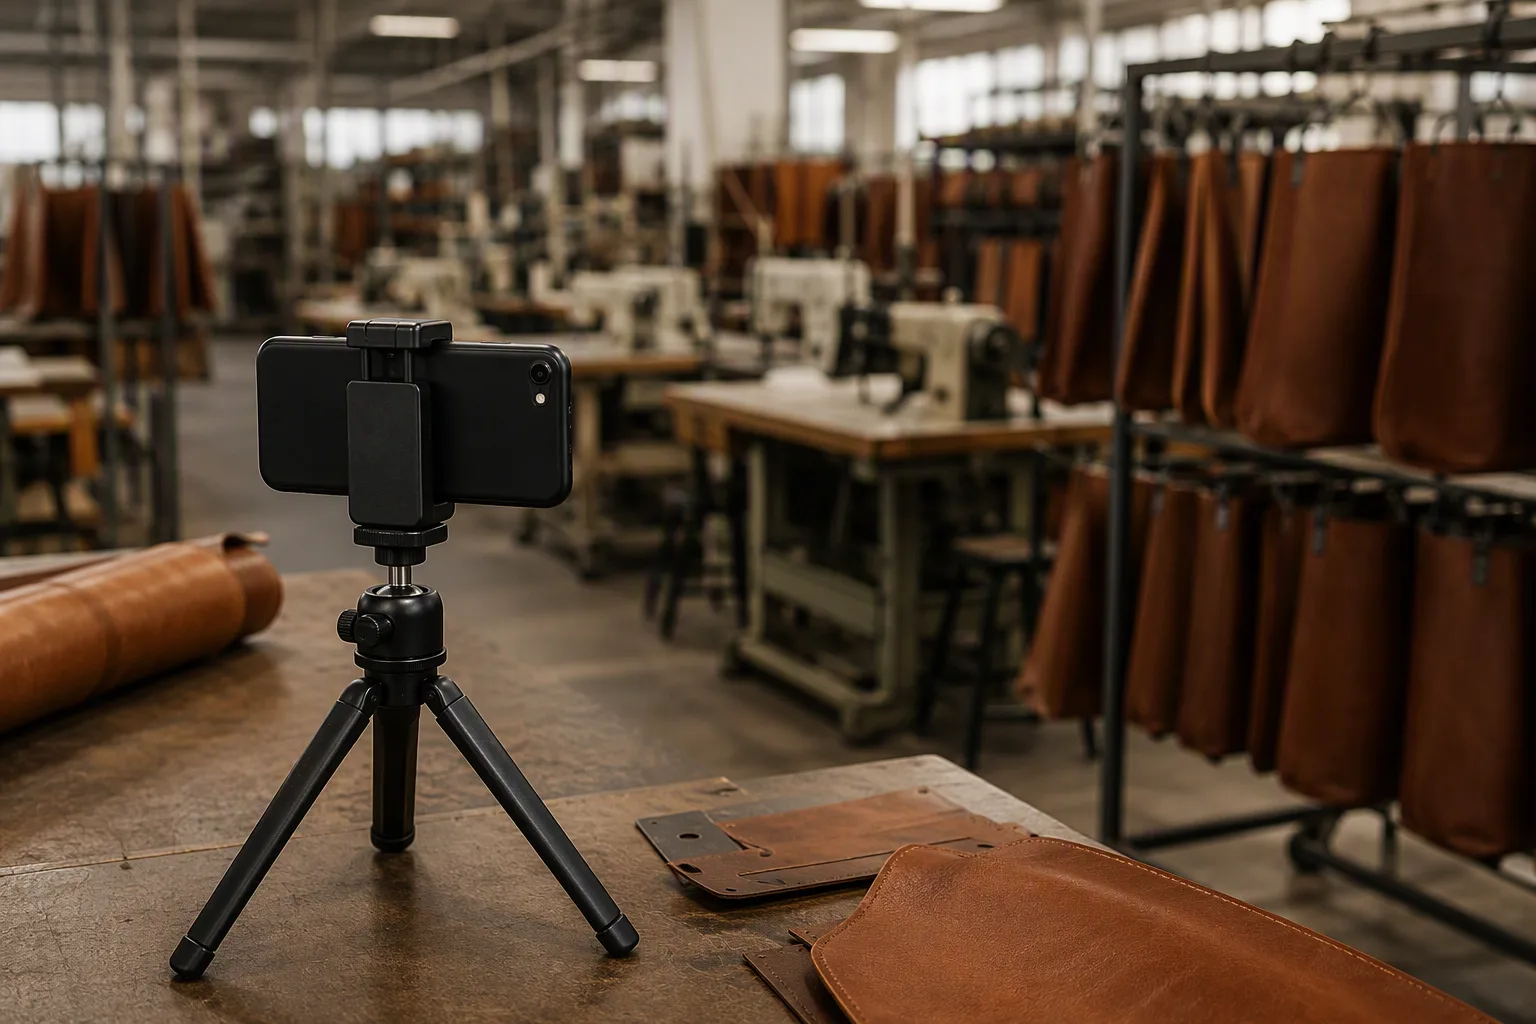
A scheduled video walkthrough with a defined route: cutting area, stitching lines, hardware application, finishing, packing, storage and quality control. Ask the factory to show specific operations live rather than sending a pre-recorded tour.
Watch the working environment rather than only the narrated content: organisation, work in progress, tool condition and whether the described process matches what appears on screen.
Live Sampling and First Article Checks
For a new product, ask for the first output of each critical operation to be shown live or photographed in detail before the batch proceeds. Catching a deviation at the first piece prevents a full batch built to the wrong standard.
Third-Party Inspection
An independent inspection before shipment provides a report that both sides can rely on, and it separates product verification from the commercial relationship. The inspection criteria should reference the approved sample and the specification, not a generic checklist.
Records to Keep
Store walkthrough recordings, first article photographs, inspection reports and sample approval records together, indexed by date and product. When a dispute arises months later, these records resolve it quickly.
The Classic Errors and How to Prevent Them
Certain mistakes recur across remote relationships, and each has a specific prevention.
| Error | How it appears | Prevention |
|---|---|---|
| Verbal change | Production differs from approval | Written change log |
| Assumed understanding | Sample built to a different intent | Written clarification summary |
| Split instructions | Factory follows the wrong requester | Single contact with authority |
| Unacknowledged messages | Work stalls silently | Explicit acknowledgement |
| Mixed feedback priorities | Minor issues fixed, major ones missed | Must-change versus optional |
| Multiple document versions | Wrong specification used | Version control |
| Approval by silence | Assumption of consent | Written confirmation |
| Late escalation | Problem discovered at shipping | Defined escalation triggers |
The Acknowledgement Habit
End every instruction with a request for confirmation, and treat silence as unconfirmed rather than agreed. A one-line reply confirming receipt and understanding closes the loop cheaply.
Escalation Triggers
Define in advance what constitutes an issue that must be raised immediately rather than at the next review: a material substitution, a schedule slip beyond a defined threshold, a defect pattern, or a deviation from the approved standard. Triggers convert vague discomfort into an actionable alert.
Managing Quality Without Being There
Remote quality management works when it depends on evidence produced by the production system rather than on the buyer's presence.
First Article Approval
The first piece of each operation should be measured, photographed and approved against the specification before the operation continues. This is the cheapest quality control available, and it is entirely compatible with remote work.
In-Process Evidence
Ask for photographs at defined stages: after cutting, after assembly of the first units, before packing. Stage photographs create a record and give early warning of drift.
Pre-Shipment Verification
The final gate is pre-shipment verification against the approved sample: dimensions, materials, hardware function, stitching, labeling and count. Where an independent inspector performs it, the report becomes the shared basis for releasing the balance payment.
Quality Data Worth Requesting
| Data point | Frequency | What it reveals |
|---|---|---|
| First article measurements | Each new operation | Setup accuracy |
| Defect count by stage | Per batch | Process stability |
| Rework records | Per batch | Hidden cost and cause |
| Material lot references | Per batch | Traceability |
| Inspection report | Per shipment | Release readiness |
When Travelling Is Worth It
Remote collaboration covers most of a sourcing relationship, but a few moments justify the cost of a visit.
Development of a Complex Product
A product with unusual construction, new hardware or demanding fit benefits from an in-person sample review, where the discussion happens over the actual object rather than photographs.
Production Start-Up
Being present for the first production run of a new design allows immediate correction and builds shared understanding of what "correct" looks like. Many brands report that one visit at this stage removes several sample rounds later.
Problem Escalation
When a defect pattern persists after written correction, presence changes the conversation. It also allows the root cause to be investigated where it occurs rather than inferred from reports.
Auditing a New Supplier
A first-time factory relationship benefits from an on-site audit, as covered in our guide to factory audits. Once the relationship is established, remote mechanisms carry the load.
Deciding Whether to Travel
| Situation | Remote adequate? | Travel justified? |
|---|---|---|
| Existing product, repeat order | Yes | Rarely |
| Minor modification | Yes | No |
| New product, familiar factory | Partly | At first production |
| New product, new factory | No | Yes |
| Persistent defect pattern | No | Yes |
Working Through Agents and Trading Companies
Many brands work with a trading company or agent rather than directly with the factory. The arrangement changes the remote dynamic and needs to be managed deliberately.
What an Agent Adds
An agent handles language, quality follow-up and factory coordination, and often holds relationships with several factories. For a brand without local presence, that can shorten the distance considerably.
The trade-off is a layer between the brand and the production floor: information passes through a filter, and technical nuance can be lost twice, once into the agent and once out of it.
Where the Layer Helps
Agents are most useful for sourcing, for routine follow-up, for consolidating orders across factories and for local problem-solving. They absorb time zone friction and handle conversations that need local context.
Where the Layer Hurts
Technical decisions suffer most. When a construction question passes through an intermediary, the answer that returns may satisfy the agent's understanding rather than the brand's requirement.
Keeping a direct channel for technical matters, with the agent informed, preserves clarity. Some brands hold technical reviews directly and use the agent for commercial coordination.
Making the Triangle Work
Define who owns what: the agent for coordination and commercial terms, the brand for specification and approval, the factory for production. State explicitly that technical approvals come from the brand.
| Arrangement | Advantage | Risk |
|---|---|---|
| Direct with factory | Clear technical channel | Time zone and language load |
| Through agent only | Low effort for brand | Filtered technical detail |
| Agent plus direct technical channel | Balance of effort and clarity | Requires clear roles |
| Brand with local staff | Maximum control | Highest cost |
Language, Translation and Visual Communication
Language is the most misunderstood variable in remote sourcing. It is not solved by finding a better translator; it is reduced by relying less on prose.
Reduce Reliance on Adjectives
Words such as soft, firm, premium or clean carry different meanings for different listeners and translate inconsistently. Replace them with measurements, references and photographs wherever a decision depends on them.
Where an adjective is unavoidable, anchor it: firm as in the approved sample, not firm in general.
Build a Shared Terminology List
A short glossary covering the terms used in the project, with the factory's own equivalent where one exists, prevents repeated misunderstanding. Add a photograph beside each term where possible.
The glossary grows with the project and becomes an asset for future orders and other factories.
Use Structured Formats
Tables, numbered lists and annotated photographs survive translation better than paragraphs. A change table with columns for element, current state, required state and priority is harder to misread than a written paragraph.
Confirm by Repetition
End a discussion by asking the other side to restate what they will do. A restatement reveals misunderstandings while they are still cheap to correct.
| Communication method | Reliability across languages | Best use |
|---|---|---|
| Long prose paragraph | Low | Background explanation |
| Numbered requirement list | High | Specifications |
| Annotated photograph | High | Visual requirements |
| Measurement table | High | Dimensions and tolerances |
| Physical sample | Highest | Reference standard |
| Restatement by receiver | High | Confirmation |
Costing and Commercial Clarity at a Distance
Remote commercial discussions drift when the basis of a number is not defined. Clarity here prevents disputes that surface at invoicing.
Defining the Basis of Every Number
Quantity tier, specification version, trade term, packaging, payment terms and validity period belong beside every price discussed. A number without its basis cannot be compared or held.
When a specification changes, the cost impact should be confirmed in writing by the factory before the change is implemented, with the revised unit cost and any tooling impact stated explicitly.
Change Costs
Changes after order confirmation carry consequences in materials, tooling and schedule. Agreeing in advance how change costs are handled avoids the common pattern where costs surface at shipment and the relationship absorbs the friction.
Invoicing Consistency
Invoice, packing list and quotation should describe the product in the same terms. Mismatches create confusion at customs and delay payment, and they undermine confidence on both sides.
| Commercial element | Must be defined with the price |
|---|---|
| Quantity tier | Yes |
| Specification version | Yes |
| Trade term | Yes |
| Packaging standard | Yes |
| Payment structure | Yes |
| Price validity | Yes |
| Change handling | Preferably |
Building Trust Without Meeting
Trust in a remote relationship is built from consistency rather than rapport. Small, verifiable behaviours accumulate.
Start Small and Verify
An initial order that tests both production capability and communication behaviour reduces risk for both sides. How a factory handles a small order predicts how it handles a large one.
Consistency Over Promises
A factory that answers within the agreed window, reports problems early and delivers what was described builds credibility faster than one that makes ambitious commitments. Track the behaviours that matter: response time, honesty about delays, adherence to approved specifications.
Transparency About Problems
Early disclosure of a problem is a positive signal, not a failure. Agree explicitly that raising an issue early is expected, and respond to it constructively rather than punitively, or the flow of early warnings will stop.
Reciprocal Commitments
Forecasts, prompt approvals and clear decisions from the brand are what allow the factory to plan. Reliability runs both ways, and factories allocate capacity to buyers who make their own commitments predictable.
| Trust behaviour | Observable signal |
|---|---|
| Response time | Answers within the agreed window |
| Problem disclosure | Issues raised early |
| Specification adherence | Production matches approval |
| Schedule reliability | Delivery dates met or flagged early |
| Documentation quality | Complete and consistent records |
A Remote Collaboration Playbook by Stage
Each stage of a project has its own remote priorities.
| Stage | Primary risk | Remote control |
|---|---|---|
| Brief and specification | Misunderstood requirement | Written clarification summary |
| Pattern making | Geometry errors | Dimensioned drawings and measurements |
| Prototype | Wrong priority in feedback | Structured numbered comments |
| Sample approval | Assumed consent | Written approval record |
| Tooling and materials | Substitution | Material references and lot checks |
| First production | Setup drift | First article approval |
| Bulk production | Undetected variation | Stage photographs and inspection |
| Pre-shipment | Release of non-conforming goods | Third-party inspection report |
| Repeat order | Silent specification drift | Versioned specification and change log |
Tools That Reduce Remote Friction
The right tools remove specific failure modes. They do not replace discipline, but they make the discipline cheaper to maintain.
Shared Documents With Versions
A shared specification document with version history removes the most common remote error: production built to a superseded version. Even a simple versioned file with a change log achieves most of the benefit.
Annotated Photography
Marking photographs removes ambiguity that text cannot reach. A circled location with an arrow and a short note communicates a requirement faster than a paragraph, and it survives translation.
Measurement Records
Recording measurements at defined checkpoints, rather than describing them in words, creates comparable data across batches. A small measurement table per batch turns quality conversations from opinions into comparisons.
A Single Project Register
One register listing open questions, pending approvals, agreed changes and their status prevents items from being lost between calls. It becomes the agenda for every review meeting.
What Each Tool Prevents
| Tool | Failure it prevents | Effort to maintain |
|---|---|---|
| Versioned specification | Production to an old spec | Low |
| Change log | Unrecorded modifications | Low |
| Annotated photographs | Misread feedback | Low |
| Measurement records | Subjective quality debate | Moderate |
| Project register | Lost open items | Low |
| Stage photograph set | Undetected process drift | Moderate |
Onboarding a New Factory Remotely
A new remote relationship deserves a deliberate ramp rather than an immediate commitment to a large order.
Capability Questions Before Commitment
Ask how the factory handles specification interpretation, sample feedback, change requests and approvals. The answers reveal whether their working method matches yours before an order is placed.
Ask also for a recent project walkthrough: what was developed, what went wrong and how it was resolved. Factories that describe problems candidly are easier to work with than ones that describe only successes.
A Deliberate First Order
A first order on an established design, at a modest quantity, tests production capability and communication behaviour together. Define in advance what would constitute success: specification adherence, schedule reliability, response quality and documentation completeness.
Structured Evaluation
Review the first order against those criteria and decide whether to expand, continue at the same level or stop. Documenting the evaluation keeps the decision based on evidence rather than impressions.
Scaling the Relationship
Where the first order succeeds, increase complexity in stages: a modification, then a custom development, then larger volumes with forecast commitments. Each stage verifies something the previous one did not.
| Onboarding stage | What it verifies | Typical duration |
|---|---|---|
| Capability discussion | Working method fit | Days |
| Sample order | Construction and finish | Weeks |
| First small order | Production and communication | One order cycle |
| Modification project | Development collaboration | One project |
| Custom development | Full capability | One season |
| Volume program | Capacity and consistency | Ongoing |
FAQ
How many sample rounds should I budget for in a remote development?
A: Two to three rounds is a reasonable planning assumption for a new pattern. Rounds are reduced by complete specifications and structured feedback, not by remote presence alone.
Is it a problem if I never visit the factory?
A: Not for routine production with an established supplier. A first production run of a new design and persistent quality problems are the two situations where presence usually pays for itself.
How often should I expect updates from the factory?
A: Define an expectation rather than waiting for one: a written progress note twice a week and a scheduled call weekly covers most projects without generating noise.
What is the single most useful document in a remote project?
A: The approved sample record, combined with the specification it was built to. It settles most disagreements about whether production matches what was agreed.
How do I give feedback when the problem is hard to describe?
A: Photograph the location with a marker, measure where a dimension is involved, and compare against the approved reference in the same lighting. Describe the required state rather than only the problem.
Should I work with an agent or directly with the factory?
A: An agent reduces language and coordination load; direct contact preserves technical clarity. Many brands combine both, with a direct channel for technical matters.
How do I prevent a factory from making changes without telling me?
A: Require written confirmation for any change, including material substitutions, and check a few specified elements against the approved standard on every batch.
What should I do when a problem is discovered only at shipment?
A: Inspect before shipment rather than after, using criteria that reference the approved sample. Once goods are in transit, the options narrow to commercial remedies.
How do I confirm that a message was actually understood?
A: Ask for a restatement of the action the factory will take. Comprehension shows up in the restatement, not in the acknowledgement.
How much documentation is too much?
A: Documentation is excessive when it goes unread. Keep the specification, the change log, the approval record and the inspection criteria current, and let the rest be disposable working notes.
Can quality be maintained remotely on a complex bag?
A: Yes, through first article approval, stage photographs and pre-shipment inspection. Complexity raises the value of each of those controls rather than making them ineffective.
What time zone practices actually help?
A: Batched question lists, a rotating meeting time so the inconvenience is shared, and a stated response window so both sides know when to expect an answer.
How do I handle a defect pattern that keeps repeating?
A: Move from correction to root cause: ask what process produces the defect, request photographs of the operation, and consider an on-site visit if the pattern persists.
Should tooling and pattern ownership be documented?
A: Yes. Record who owns the pattern and tooling, where they are stored and what happens if the relationship ends. This is cheapest to settle before development begins.
What is a reasonable first order to test a new factory remotely?
A: A small order of an established design tests production capability and communication behaviour at low risk. Reserve custom development for factories that have demonstrated both.
How do I keep a repeat order aligned with the original specification?
A: Keep a versioned specification with a change log, and confirm the current version at each order. Silent drift between seasons is one of the most common remote failures.
Ready to make your remote factory relationship work reliably? Share your product, your factory location and the stage you are at, and we will help you build the handoff documents, feedback structure and inspection cadence that keep an overseas project on schedule and on specification.