Leather Printing vs Embossing: Decorating Techniques Compared
- Decoration Methods at a Glance
- How Embossing and Debossing Work
- Printing Techniques: Hot Stamping, Screen and Digital
- Tooling Requirements and Development
- Durability and How Each Method Wears
- Design Suitability
- Cost Drivers
- Quality Control for Decorated Leather
- Specifying Decoration in a Tech Pack
- Combining Methods
- Decoration and Leather Sourcing
- Production Scale and Decoration Consistency
- Where the Mark Goes
- Personalisation and Variable Data
- Common Misconceptions About Decoration
- In-House Decoration Versus Outsourcing
- FAQ
A bag carries two kinds of decoration: the kind that sits on the surface, and the kind that becomes part of the leather. Printing techniques apply material to the hide; embossing and debossing reshape it. The distinction decides how long the decoration survives, what tooling it requires, and whether the design is even achievable.
Brands often arrive at the factory with a design that looks straightforward on screen and discover that the combination of line weight, leather temper and finish makes it impossible to produce reliably. Most of those problems are avoidable, because each decoration method has known limits that can be checked before tooling is cut.
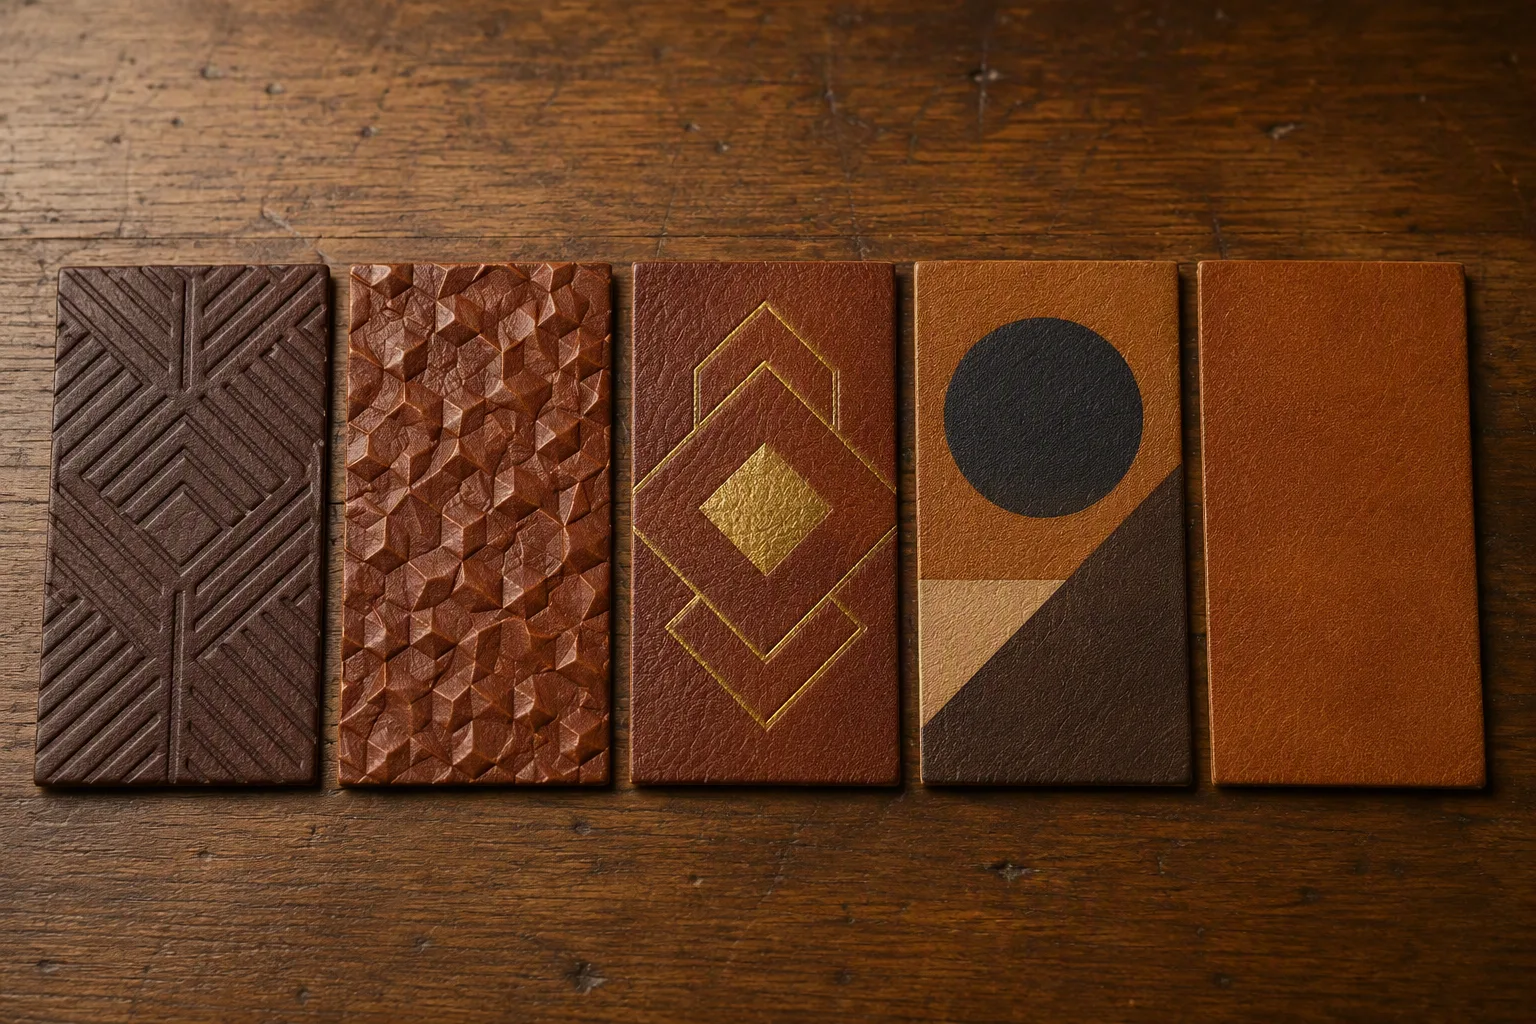
This guide compares the main options on leather bags: hot foil stamping, screen printing, digital printing, embossing and debossing, laser engraving and stitched or appliquéd elements. It covers how each process works, what tooling it needs, how it wears, what it costs to set up and run, which designs suit it, how factories inspect decorated leather, and how to specify decoration in a tech pack.
Decoration Methods at a Glance
The available methods divide into surface decoration and structural decoration, and the division predicts most of their behaviour.
Surface Decoration
Hot foil stamping, screen printing and digital printing all add a layer to the leather surface. That layer carries the visual effect, whether metallic, matte, coloured or photographic.
Because the effect lives in an applied layer, its durability depends on adhesion and abrasion resistance rather than on the leather itself. Surface decoration is also the only route to multi-colour and photographic results.
Structural Decoration
Embossing, debossing and laser engraving change the leather physically. The design exists as a raised or recessed shape in the material, and it therefore ages with the hide rather than wearing off it.
The trade-off is design freedom: colour is limited to the leather and to any finish applied after forming, and fine detail is constrained by how precisely the leather will hold a shape.
Where Each Method Fits
| Method | Type | Colour capability | Typical use |
|---|---|---|---|
| Hot foil stamping | Surface | Single or multi-foil | Logos, lettering |
| Screen printing | Surface | Multiple colours | Graphic prints |
| Digital printing | Surface | Full colour | Photographic and complex art |
| Embossing | Structural | Tone on tone | Logos, patterns |
| Debossing | Structural | Tone on tone | Discreet branding |
| Laser engraving | Structural | Tone or burn tone | Fine detail, personalisation |
| Stitching and appliqué | Neither | Multi-material | Panels and emblems |
How Embossing and Debossing Work
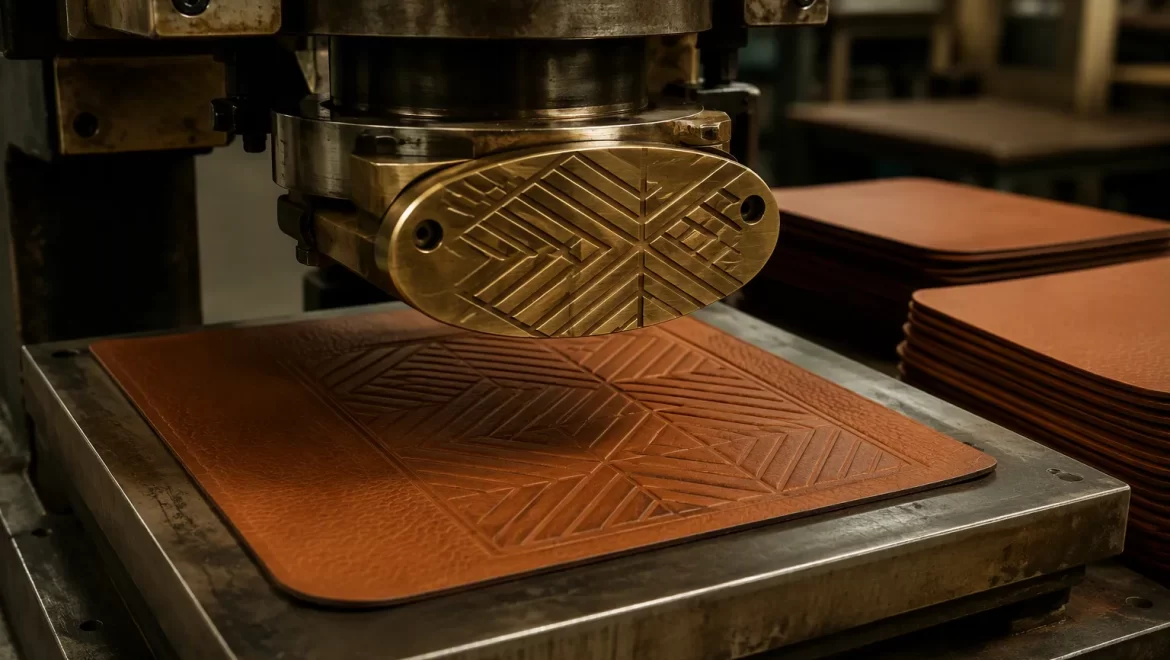
Embossing raises the design above the surface; debossing presses it below. Both rely on the same mechanics: a shaped die, heat, pressure and time.
Dies, Heat and Pressure
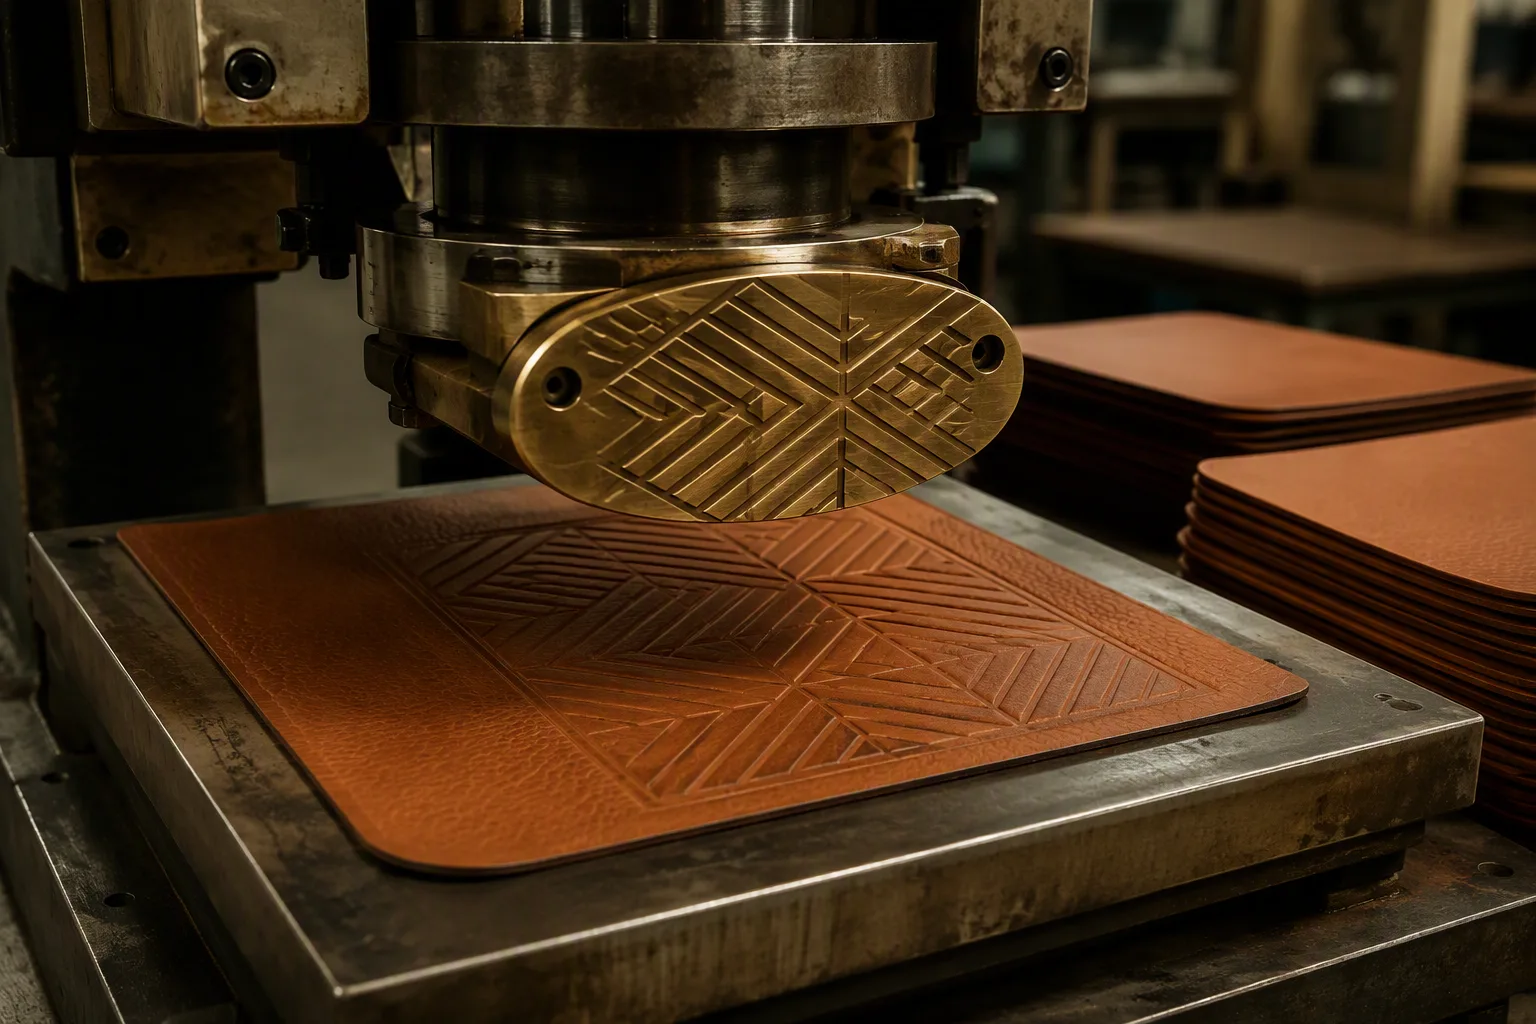
A metal die carrying the mirrored design is mounted in a press and heated. The leather is positioned, the press closes, and the combination of temperature, pressure and dwell time transfers the shape into the hide.
Deeper impressions need more of all three, but leather has limits. Push too far and the fibres crush, the grain splits, or the shape recovers partially after the press opens, leaving a soft impression that loses definition.
How Leather Affects the Result
Three properties determine how a hide takes an impression: tannage, temper and surface finish.
Vegetable-tanned leathers with a firm temper hold crisp, deep impressions and age attractively as the raised areas darken. Soft, chrome-tanned leathers tend to produce shallower impressions with softer edges. Heavily finished leathers with a thick surface coating can crack or delaminate when pressed, because the coating does not stretch with the fibres beneath it.
Controlling Definition
Definition is controlled by die quality, temperature, pressure, dwell time and a cooling period before the leather is moved. A factory that rushes the cooling stage produces impressions that look correct on the bench and soften within days.
Where a design is deep, the die may be made in stages or the leather may be conditioned before pressing to reduce the risk of cracking.
Where Each Embossing Variant Suits
| Variant | Depth | Best on | Risk |
|---|---|---|---|
| Fine deboss | Shallow | Firm finished leather | Low |
| Deep deboss | Deep | Vegetable-tanned, firm | Grain cracking |
| Emboss (raised) | Moderate | Firm leather, structured panels | Flattening over time |
| Multi-level emboss | Varied | Firm leather, decorative panels | Die cost |
| Textured emboss | Surface wide | Any firm leather | Inconsistent depth |
Printing Techniques: Hot Stamping, Screen and Digital
The printing family is broader than most buyers expect, and the three main processes serve different design needs.
Hot Foil Stamping
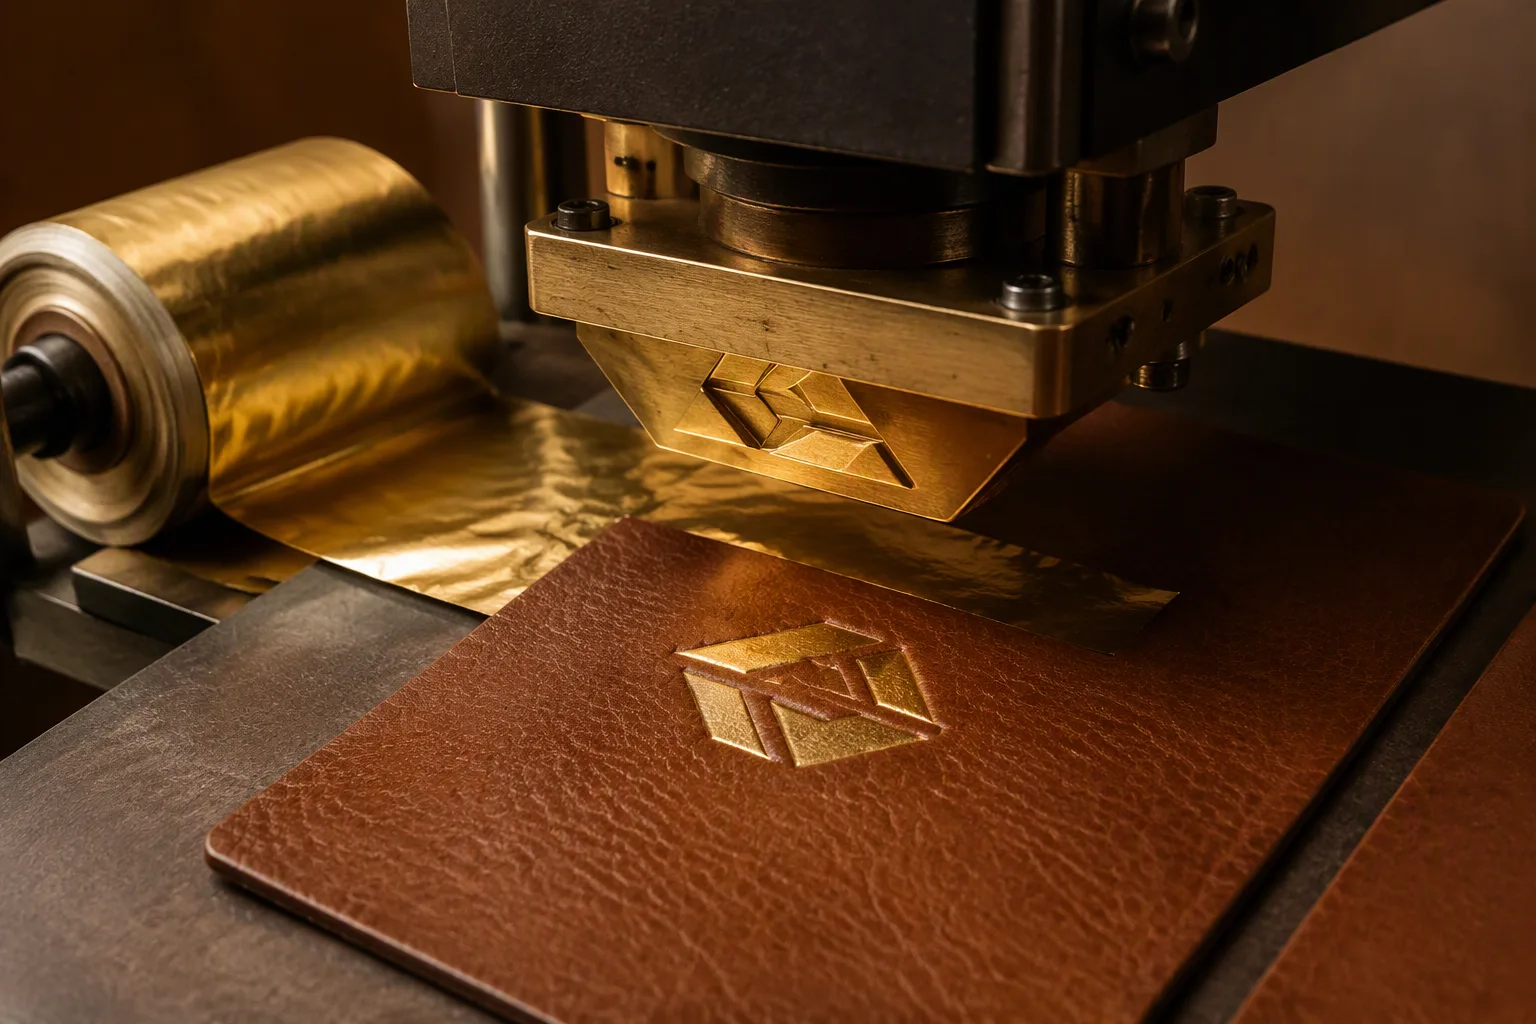
A heated die presses a thin foil against the leather, transferring the foil's colour and finish into the impression. Metallic, matte, gloss, pigment and holographic foils are available.
Hot stamping produces a crisp, high-contrast mark that reads as premium on a dark hide. Its weakness is abrasion: foil is a layer, and layers can wear. Adhesion depends on the leather finish, the foil grade and the press settings, which is why the same foil behaves differently across suppliers.
Screen Printing
Ink is pushed through a mesh screen onto the leather and then cured. Each colour requires its own screen, so the process scales in cost with the number of colours rather than with the quantity.
Screen printing suits graphic designs, flat colour blocks and larger motifs where a slightly raised ink layer is acceptable. On soft or stretchy leathers, the printed areas can crack if the bag flexes repeatedly.
Digital Printing
Digital printing applies ink directly without a screen or die, which makes it the only practical route to photographic imagery and gradients on leather. Setup cost is minimal, so it suits short runs and personalised pieces.
Durability is the trade-off. Ink sits on the surface and can abrade or fade, and on leather with a heavy finish the ink may not key reliably. Digital printing is usually paired with a protective top coat on areas that will be handled constantly.
Comparing the Printing Options
| Process | Setup requirement | Colour range | Abrasion resistance | Best use |
|---|---|---|---|---|
| Hot foil stamping | Metal die | Foil colours | Moderate | Logos and lettering |
| Screen printing | One screen per colour | Flat colours | Moderate | Graphic motifs |
| Digital printing | File preparation | Full colour | Lower | Photographic art |
| Foil plus emboss | Die plus foil | Foil colours | Higher | Premium branding |
Tooling Requirements and Development
Tooling is the fixed cost of decoration, and it is where most schedule surprises originate.
Die Types
Metal dies are the standard for both embossing and hot stamping. Brass is common for hot stamping because it conducts heat evenly; steel and magnesium appear where deeper impressions or higher volumes justify the cost and weight.
For embossing, the die may be engraved directly or built as a mould for a matching set where both sides of the leather are formed.
Development Cycle
Die production usually runs from several days to a couple of weeks depending on complexity and the engraving method. The die must be cut from artwork prepared to the process, then tested on the actual leather before production.
Testing on a representative hide matters more than testing on a scrap, because tannage and finish change the result as much as the die does.
Artwork Preparation
Artwork must be vector-based, with line weights above the process minimum, adequate spacing between fine elements, and no hairlines or tight negative spaces that will fill in under pressure or bleed in print. Text below a certain size loses legibility in embossing and can fill with foil in stamping.
| Element | Embossing requirement | Printing requirement |
|---|---|---|
| Line weight | Above the minimum for the depth | Above ink bleed threshold |
| Negative space | Generous | Adequate for ink spread |
| Text size | Larger than print minimum | Smaller text possible |
| File format | Vector artwork | Vector preferred |
| Depth specification | Stated in millimetres or by die depth | Not applicable |
| Proofing | Press test on production leather | Sample print run |
Durability and How Each Method Wears
Durability differences show up in different ways for each family, and buyers who understand the failure mode can specify accordingly.
Embossed Decoration
Because the shape is formed in the leather, embossed decoration does not peel or flake. Its risks are definition loss over time as the leather relaxes, and darkening or lightening of the formed areas as the leather patinas.
On firm vegetable-tanned leather, an impression can remain sharp for the life of the bag. On soft leather, the same impression may soften noticeably within a season.
Foil and Print Wear
Foil and ink sit on the surface and are affected by friction. The locations that fail first are those that contact hands, clothing or hard surfaces: around openings, on pocket fronts and along edges.
Adhesion testing on production leather, plus attention to where the decoration is placed relative to wear points, does more for durability than upgrading the foil alone.
Comparing Wear Behaviour
| Decoration | Primary failure mode | Where it fails first | Mitigation |
|---|---|---|---|
| Emboss | Definition loss | Soft leather, flexible areas | Choose firm leather, limit depth |
| Deboss | Softening | Repeated flex points | Reduce flex, condition leather |
| Hot foil | Abrasion | Handle and opening areas | Better foil grade, top coat |
| Screen print | Cracking, ink wear | Flexing panels | Elastic ink, limit stretch |
| Digital print | Fading, abrasion | Contact areas | Protective top coat |
| Laser engraving | Charred edges, uneven tone | Fine detail | Parameter tuning per leather |
Design Suitability
Not every design works in every medium, and the constraints are specific enough to plan around.
Line Weight and Small Text
Fine lines behave differently in each process. In embossing, a very fine line produces a shallow impression that disappears in soft leather. In screen printing, it can fill with ink. In hot stamping, it can smear if the foil is over-pressured.
As a working rule, the smaller and finer the design, the more the decision should be driven by leather properties rather than by artwork alone.
Leather Colour and Finish
Contrast drives perception of a decoration. Tone-on-tone embossing on firm vegetable-tanned leather reads through shadow and patina, while the same design on a dark, heavily finished leather may be invisible.
Foil and ink solve contrast problems, but they also introduce adhesion risk on heavily finished surfaces. Where the surface is coated, adhesion testing is essential before committing to a run.
Placement and Curvature
Decoration on a flat panel behaves predictably. Decoration across a curve, a seam or a gusset requires either a shaped die or a printing method that can follow the surface.
Placement near edges also risks distortion during folding and edge finishing, so the decoration should sit clear of operations that will move the leather.
Colour and Complexity
Multi-colour work belongs to screen and digital printing. Multi-level relief belongs to embossing. Designs that require both depth and colour usually combine a deboss with a foil, a process that costs more but produces the most dimensional result.
Cost Drivers
Decoration cost has two components: a one-time tooling and development charge, and a per-piece processing cost. Their relative weight changes with volume.
One-Time Costs
Die engraving, artwork preparation and press testing form the fixed cost. Complexity drives it: fine detail, large areas and multi-level dies all cost more than a simple deboss.
Screen printing swaps die cost for screen cost per colour, and digital printing removes tooling almost entirely.
Per-Piece Costs
Per-piece cost reflects machine time, operator time, consumables such as foil or ink, and yield. Deep embossing takes longer per piece than a light deboss, and foil stamping adds the cost of the foil itself, which is consumed rather than reused.
How Volume Changes the Balance
At low volumes, tooling dominates and process choice should favour low setup. At high volumes, per-piece cost dominates and the cheaper tooling option may be the more expensive one overall.
| Cost element | Emboss | Hot foil | Screen | Digital |
|---|---|---|---|---|
| Tooling | Die | Die | Screens | None |
| Artwork preparation | Required | Required | Required | Required |
| Consumables | None | Foil | Ink | Ink |
| Cycle time | Moderate to high | Moderate | Moderate | Low |
| Setup per run | Low | Low | Moderate | Minimal |
| Favours | Any volume | Any volume | Medium to high | Low to medium |
Quality Control for Decorated Leather
Decoration inspection is part visual, part physical. Both belong in the quality plan, because some failures only appear after use.
Visual Checks
Check position against the specification, definition of the impression, consistency between pieces, absence of double impressions, and cleanliness of the surrounding surface. Position errors are the most common defect because decoration is often applied after assembly.
Physical Checks
Adhesion tests for foil and print, abrasion tests for surface decoration, and flex tests for printed areas that will move with the bag. On embossed leather, check that the depth is consistent and that the grain has not cracked at the edges of the impression.
Common Defects
| Defect | Method affected | Cause | Prevention |
|---|---|---|---|
| Weak impression | Emboss | Low pressure or temperature | Press settings on production leather |
| Grain cracking | Emboss | Depth too great for the leather | Depth test, pre-conditioning |
| Foil flaking | Hot foil | Poor adhesion, wrong foil grade | Adhesion test, foil matching |
| Ink filling fine lines | Screen | Ink viscosity, screen mesh | Mesh and viscosity control |
| Position drift | All | Manual placement | Fixture or jig |
| Charred edges | Laser | Parameters unsuited to the leather | Parameter tuning per hide |
Specifying Decoration in a Tech Pack
Decoration specifications are frequently vague, and vagueness here produces expensive rework because the error surfaces after assembly.
Defining the Element
State the method, the position with dimensions from defined reference points, the size, the colour or finish reference, and the depth where the process forms the leather. Include a visual reference of the intended result.
Files and Tolerances
Provide vector artwork at the correct scale, plus a proof showing the intended appearance on the actual leather colour. State the acceptable positional tolerance, typically in millimetres, and whether minor depth variation is acceptable.
Sample Approval
Approve decoration on a sample built from production leather with production tooling. A proof printed on paper does not predict how the impression will read on a grained or dark hide.
Specification Checklist
| Item | Must be specified |
|---|---|
| Method | Yes |
| Position and reference points | Yes |
| Size | Yes |
| Depth | Where formed |
| Colour reference | For surface methods |
| Artwork files | Yes |
| Tolerance | Yes |
| Proof on leather | Required |
| Inspection criteria | Yes |
Combining Methods
Most decorated bags use more than one technique, and the combinations are where design intent is realised.
Deboss with Foil
Stamping a coloured or metallic foil into a debossed impression produces the highest perceived quality in branding: the mark is both formed and coloured. It costs more than either process alone but survives wear noticeably better than a foil mark on a flat surface.
Embossed Pattern with Printed Accent
A textured or pattern-embossed panel combined with a printed or foiled accent lets the design carry both surface interest and specific detail. The pattern is set at the leather stage, the accent applied after assembly.
Laser Detail with Structural Elements
Laser engraving can add fine detail without tooling, which suits personalisation and short runs. Its parameters must be tuned to the hide, because the same settings produce different tones across tannages.
Decoration and Leather Sourcing
Decoration requirements belong in the leather conversation, not after it. The hide chosen for its colour and hand feel may be the one that refuses to hold an impression.
Matching the Hide to the Method
A firm vegetable-tanned leather is the natural partner for deep embossing, while a heavily coated finished leather suits foil stamping that keys to the coating rather than the fibres. Soft chrome-tanned hides take light debossing well and resist deep impressions poorly.
When a brand wants both a specific hand feel and a deep formed mark, the resolution is usually a different construction: a firm panel for the decorated element, laminated or stitched to a softer body.
What to Ask a Leather Supplier
Ask how the hide behaves under heat and pressure, whether the finish is suitable for foil or ink adhesion, and whether other buyers use it for embossed work. A supplier who has seen the hide decorated before can save several test rounds.
Ask also for the finish specification: coated, aniline, semi-aniline or pigmented. The finish type predicts adhesion far better than the colour or grain description.
Trial Before Commitment
Test decoration on production leather before ordering tooling in volume. A single test press on a representative hide reveals whether the impression holds, whether the grain cracks and how the foil or ink behaves.
| Leather type | Emboss suitability | Foil adhesion | Digital ink keying |
|---|---|---|---|
| Vegetable-tanned, firm | Excellent | Good | Moderate |
| Chrome-tanned, soft | Moderate | Good | Moderate |
| Pigmented finish | Poor for deep work | Good | Variable |
| Aniline, uncoated | Good | Moderate | Difficult |
| Coated, embossed grain | Poor for deep work | Variable | Poor |
Production Scale and Decoration Consistency
A decoration that looks correct on one sample can drift across a production run. Consistency comes from fixtures, parameters and verification rather than from operator attention.
Fixtures and Placement
Hand placement produces variation. A simple fixture that locates the panel relative to the die removes most positional error and speeds the operation at the same time.
Where the decorated element is small and repeated many times per bag, the fixture also protects the surrounding leather from stray impressions.
Parameter Control
Temperature, pressure and dwell time should be recorded as production settings and verified at the start of each shift. Small temperature changes produce visible differences in foil release and impression depth.
Consumables matter too: foil grade and lot, ink viscosity and screen condition all change output. Recording the consumable specification alongside the settings makes a repeat order reproducible.
Consistency Across Batches
Between batches, leather lots change and so does the output. Keeping a reference sample from the approved run, and comparing new output against it, catches drift before a shipment is packed.
| Consistency risk | Source | Control |
|---|---|---|
| Position drift | Manual placement | Fixture or jig |
| Depth variation | Temperature and pressure | Recorded settings, shift checks |
| Foil release difference | Foil lot | Material lot records |
| Colour shift | Ink batch, screen wear | Reference sample comparison |
| Hide variation | Tannage and finish lot | Incoming leather inspection |
Where the Mark Goes
Placement shapes how the decoration is perceived and how it wears, and both considerations point in the same direction more often than expected.
Panel Placement Versus Hardware Placement
Decoration on a flat panel is straightforward to apply and predictable in wear. Decoration on or near hardware introduces curvature, thickness variation and contact with metal.
Where a design calls for both, the practical sequence is to decorate the panel before hardware is set, allowing the panel to be supported flat during pressing.
Interior Marking
Debossed branding on an interior panel is common because it survives heavy use and requires no additional material. It also avoids the abrasion that exterior marks on handled surfaces eventually experience.
Interior placement requires the lining to be firm enough to hold an impression; soft fabrics and stretch linings will not.
Wear Points to Avoid
Places that contact hands, clothing, seats or sharp edges will show wear on any surface decoration. Positioning a foil or printed mark away from those zones extends its life without changing the process.
Placement Guidance
| Location | Suitability | Note |
|---|---|---|
| Front panel centre | High | Flat, visible, low wear |
| Front panel lower corner | Moderate | Contact with surfaces |
| Near handle root | Lower | Flex and contact |
| Interior panel | High | Durable, discreet |
| Gusset or side | Moderate | Curvature complicates pressing |
| Strap end | High | Small area, low wear if laid flat |
Personalisation and Variable Data
Personalised products command higher prices and suit methods that do not require a dedicated die per design.
Laser Engraving for Variable Content
Laser engraving produces no tooling cost, so initials, names and short text can vary per unit. Its limits are tonal: engraved areas appear darker or lighter depending on the hide, and achieving a consistent look across leather types requires parameter tuning.
Digital Printing for Variable Artwork
Digital printing removes both tooling and screen cost, which makes it viable for short runs and artwork that changes between orders. The durability trade-off discussed earlier still applies, and a protective finish extends service life on handled surfaces.
Hot Stamping with Changeable Type
Hot stamping can incorporate interchangeable type for initials, keeping the premium metallic look while allowing variation. It suits small character counts rather than full variable graphics.
Choosing for Variable Work
| Method | Tooling per variation | Suitable content | Wear profile |
|---|---|---|---|
| Laser engraving | None | Initials, short text | Good |
| Digital printing | None | Full artwork | Moderate |
| Hot stamping with type | Type sets | Initials, dates | Moderate |
| Embossing | Die per design | Fixed designs only | Best |
Common Misconceptions About Decoration
Several assumptions drive buyers toward methods that cannot deliver what they expect.
"Any Leather Can Take a Deep Emboss"
Depth depends on tannage, temper and finish. Soft hides accept a shallow impression; heavily coated hides may crack. Depth is a property of the material pair, not a setting on the press.
"Foil Never Wears Off"
Foil is an applied layer and will abrade on contact surfaces. Adhesion can be improved with foil grade, press settings and a top coat, and placement can avoid the heaviest wear, but the layer remains a layer.
"Digital Printing Is the Cheapest Option"
Digital printing removes tooling, which makes it cheapest at low volumes and for variable content. Per-piece cost is not the lowest, and durability may require additional finishing.
"Decoration Can Be Decided After Sampling"
Decoration affects leather choice, panel construction and tooling. Deciding after sampling frequently forces a change of leather or a redesign of the decorated element, both of which cost more than deciding early.
In-House Decoration Versus Outsourcing
Not every bag factory decorates in-house. Understanding who performs the operation, and how the handover is controlled, prevents a common source of delay and rework.
When Factories Decorate In-House
Factories with steady decoration volume usually keep press equipment on site, which shortens the cycle and keeps the decorated panels under their own quality control. In-house work also makes it easier to correct a defect before assembly.
When the Work Is Outsourced
Specialists often handle foil stamping, screen printing or laser engraving, particularly where the factory's volume does not justify the equipment or where the process requires specialist dies and consumables.
Outsourcing adds a transport step and a handover point, both of which introduce risk: panels can be mixed between orders, and a defect may only be discovered when the panels return.
Controlling the Handover
Send panels in labelled batches with the artwork, the leather reference and the required position marked. Ask for the first piece to be photographed and confirmed before the batch proceeds, and require the returned pieces to be checked against the approved sample.
Where decoration is critical to the product's identity, inspect the returned panels before assembly rather than relying on final inspection, because a decorated panel that fails is harder to replace once the bag is built.
Deciding Between the Two
| Factor | In-house | Outsourced specialist |
|---|---|---|
| Cycle time | Shorter | Longer with transport |
| Process depth | General capability | Specialised capability |
| Cost at low volume | Lower setup | May be higher |
| Quality control | Within the factory | Requires handover checks |
| Risk | Lower | Panel mixing and transport damage |
| Best for | Standard branding work | Complex or specialist decoration |
FAQ
How deep can an embossed logo go on a leather bag?
A: Depth depends on the leather rather than a fixed limit. Firm vegetable-tanned hides take a deep, crisp impression; soft or heavily coated hides take a shallow one. Test on production leather before cutting dies.
Which lasts longer, foil stamping or embossing?
A: Embossed decoration lasts longer because it is formed in the leather rather than applied to it. Foil can be made durable with the right grade, settings and placement, but it remains a surface layer.
Can I emboss a design with multiple colours?
A: Embossing produces no colour of its own. Multi-colour work requires printing, or a combination of debossing with a foil or ink fill.
How long does die production take?
A: Depending on complexity and the engraving method, die production typically takes several days to a couple of weeks, plus test pressing on production leather before the run.
Is screen printing suitable for small quantities?
A: Each colour requires its own screen, so setup cost is fixed per colour. It suits medium to larger runs better than short ones.
Will foil stamping hold on a pigmented or coated leather?
A: Adhesion depends on the coating. Coated surfaces can hold foil well when the grade and press settings match, but testing is essential because performance varies between finishes.
Can decoration be applied after the bag is assembled?
A: It can, but the bag is harder to support flat and position accurately. Where possible, decorate the panel before assembly and before hardware is set.
What is the minimum text size for embossing?
A: There is no universal figure; the limit depends on leather, depth and die quality. Fine serifs and hairlines fill in or disappear first, so simple, open letterforms hold up best.
How do I keep decoration position consistent across a production run?
A: Use a fixture that locates the panel against the die rather than relying on hand placement, and record the press settings so each shift starts from the same parameters.
Does decoration affect the leather I can choose?
A: Yes. Decoration requirements constrain tannage, temper and finish, and it is cheaper to select leather with the method in mind than to change leather after sampling.
What should I check on a decorated sample?
A: Position against the specification, definition and depth, appearance on the actual leather colour, adhesion or abrasion behaviour where relevant, and consistency across several pieces.
Is laser engraving suitable for brand logos?
A: It suits fine detail and variable content without tooling, but the tonal result varies with the hide. Consistency across leather types requires parameter tuning per material.
Can I combine embossing and foil stamping in one operation?
A: Where the die is designed for it, a foil can be stamped into an embossed impression in a single press. This produces the most dimensional and durable branding result.
How do I test durability before committing to production?
A: Request an abrasion test on foil or print and a flex test where the decorated area will move. On embossed leather, check for grain cracking at the impression edges after flexing.
Does decoration add much to unit cost?
A: Setup is the dominant cost at low volumes; consumables and machine time dominate at high volumes. Deep embossing and foil stamping cost more per piece than a light deboss.
What artwork format does a factory need?
A: Vector artwork at the correct scale, prepared with line weights above the process minimum and adequate spacing between fine elements. A proof on the actual leather should follow.
Ready to choose the right decoration method for your bag line? Share your design, the leather you plan to use and your expected volumes, and we will help you match the process to the material: embossing and debossing where the mark should last as long as the bag, printing where colour and complexity matter more than depth, and combined techniques where the product needs both.