How Do You Assess a Bag Factory's Real Capacity?
- Why Quoted Capacity Is Not Real Capacity
- The Unit Problem: What Capacity Actually Measures
- Counting the Floor: Workstations and Direct Labour
- Takt Time and the Rhythm of a Line
- Finding the Bottleneck
- Efficiency, Attendance and the Realistic Hour
- Peak Season Occupancy and Calendar Loading
- Outsourcing Ratios and What They Hide
- Material and Component Constraints on Capacity
- Sampling, Development and Pre-Production Load
- Verifying the Claim: The Walk-Through Assessment
- Documents Worth Asking For
- Trial Orders and Capacity Probes
- Red Flags in Capacity Conversations
- Structuring a Capacity Agreement
- Capacity for Growth: What Headroom Costs
- Frequently Asked Questions
- What to Do Before the Next Quotation Arrives
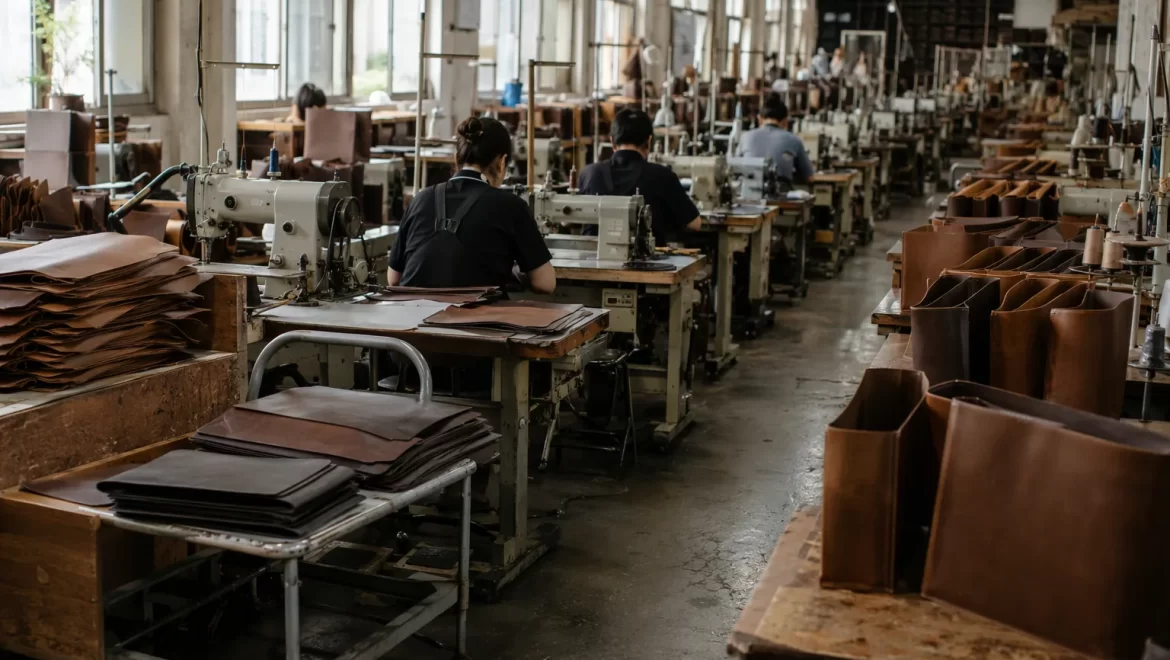
Every bag factory has two capacity figures. One is the number that appears in the quotation and the audit form: a round, confident statement of monthly output. The other is the number that emerges when you stand on the floor at four in the afternoon on a Thursday in September, count who is actually working, time the operation that everything queues behind, and subtract the orders that were promised before yours.
The first number is a marketing document. The second is a production constraint. Buyers who plan on the first number discover the difference in the third week of a peak season, when the line they were told would run at eight hundred pieces a day is producing five hundred and the reason is not negligence but arithmetic.
Capacity is not a claim to be believed or doubted. It is a quantity to be measured, and it can be measured before a purchase order exists. What follows is how a bag manufacturer assesses real capacity — our own and, by extension, what a buyer should require of any factory under consideration — from the unit of measurement through to the verification methods that separate a capacity commitment from a capacity hope.
Why Quoted Capacity Is Not Real Capacity
A quoted capacity is usually produced by multiplying a theoretical daily output by working days, then rounding upward. The theoretical daily output comes from a line configuration that may have existed when the factory was smaller, or from the best day the line ever had, or from a competitor's brochure.
Three distortions are almost universal.
The mix distortion. A factory that quotes 30,000 pieces a month is quoting a number that only holds for a particular product mix. Thirty thousand simple tote bags and thirty thousand structured laptop bags do not come from the same line at the same rate. If the quotation does not specify the reference product, the number has no operational meaning.
The denominator distortion. Monthly output divided by thirty days assumes the factory works every day. Many workshops work twenty-six days, and during national holidays fewer. Some run two shifts on cutting and one on assembly. A capacity figure without a shift calendar and a working-day count is a shape, not a size.
The occupancy distortion. A factory at seventy percent committed has thirty percent to offer. A factory at ninety-five percent committed has five percent, and that five percent is not available in the month you need it — it is available in the gaps between other customers' shipments, which are unpredictable and frequently consumed by rework.
Real capacity, for planning purposes, is the output a specific line can sustain for a specific product over a specific calendar window, after deducting committed load, expected absent days, rework, and the pre-production work your own order will consume.
The Unit Problem: What Capacity Actually Measures
Before counting anything, fix the unit. Factories and buyers routinely compare numbers that are not commensurable, and most capacity disputes are unit disputes wearing a scheduling costume.
Four units appear in practice: pieces per day, which is the common claim and the most sensitive to product complexity; standard minutes per piece, the operation time content that converts cleanly into labour hours; machine hours, meaningful for cutting, skiving and embossing but not for hand assembly; and line-days, a booking unit that says nothing about what runs on the line.
The only unit that supports honest comparison across products is the standard minute, because it ties output to labour content. A factory that can deliver 4,800 standard minutes of assembly work per day per line will produce 600 pieces of an eight-minute bag, 400 pieces of a twelve-minute bag, and 240 pieces of a twenty-minute bag. The same capacity produces three different piece counts. Any quotation that states only pieces has hidden the conversion.
Ask for the standard minute value of the reference product used to derive the quoted capacity. If the factory cannot state it, the quoted figure was not derived from a time study, and it should be treated as an aspiration.
| Unit | What it measures | Useful for | Weakness |
|---|---|---|---|
| Pieces per day | Output of a defined product | Order scheduling | Collapses under mix change |
| Standard minutes per piece | Labour content | Cross-product comparison | Requires a real time study |
| Machine hours | Machine occupancy | Cutting, skiving, embossing | Ignores hand operations |
| Line-days | Reserved assembly time | Booking and contract terms | Silent on product complexity |
Counting the Floor: Workstations and Direct Labour
Capacity begins with a headcount that can be verified. Not the payroll headcount, not the headcount on the company profile, but the number of people physically seated at workstations doing production work on the day of the assessment.
Walk the floor and count stations by operation. A bag factory typically contains these operational clusters:
- Cutting (die press, straight knife, band knife)
- Skiving and edge preparation
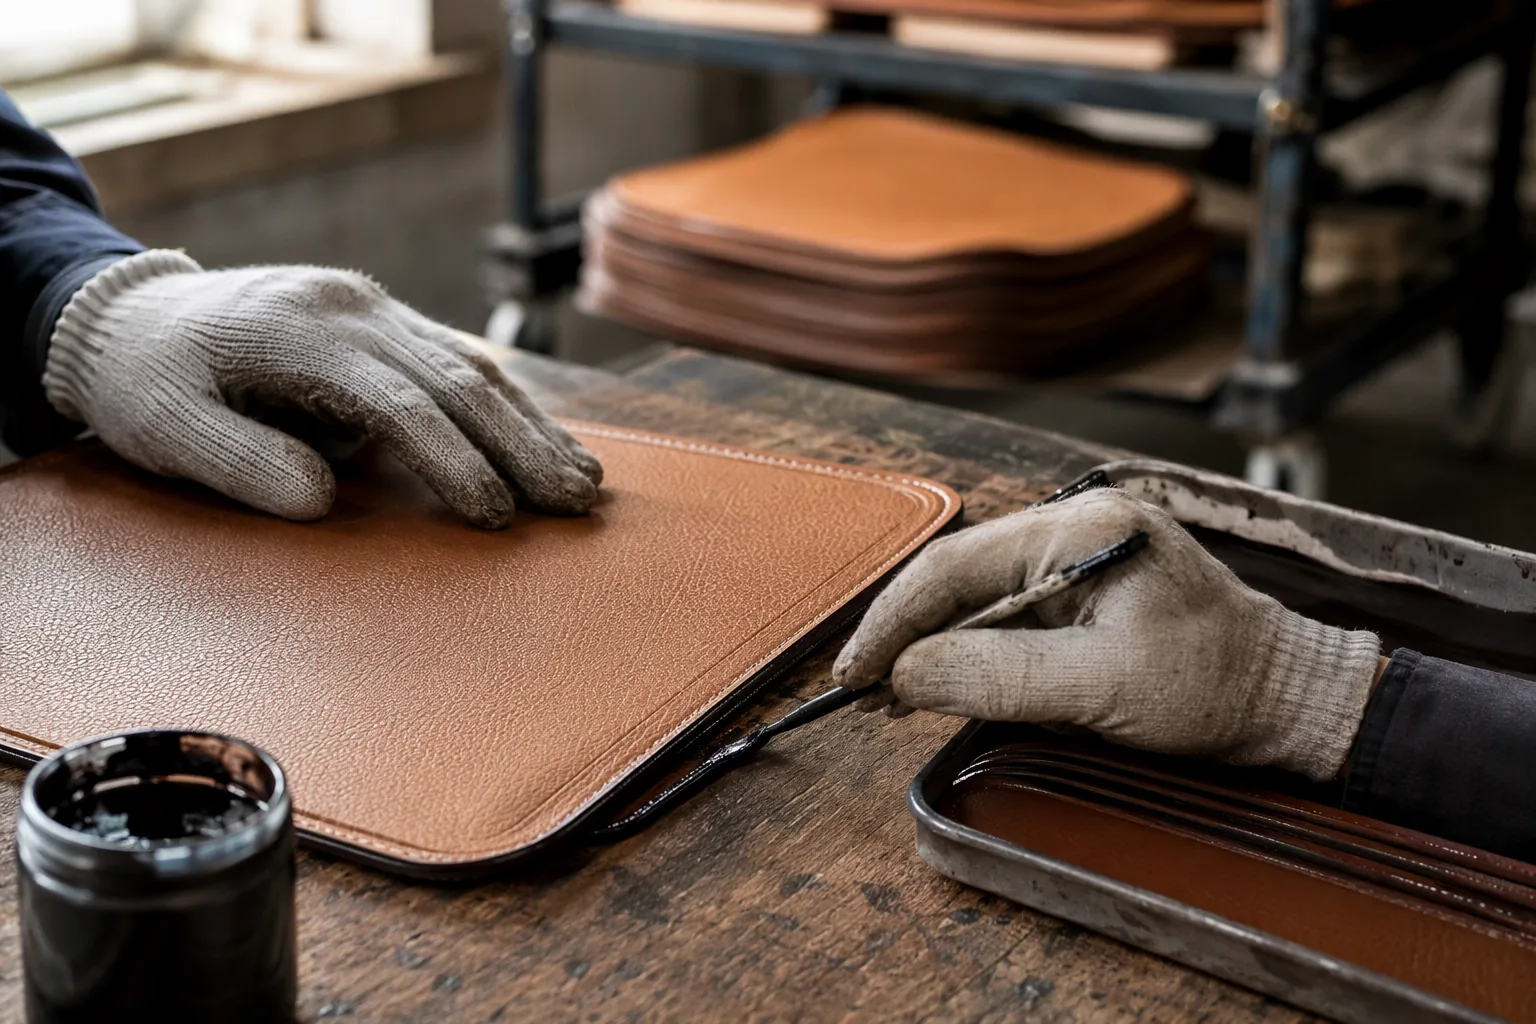
- Edge painting or edge folding
- Sewing — flatbed, post-bed, cylinder-arm, heavy-duty
- Hardware setting and riveting
- Zipper assembly
- Lining and sub-assembly
- Turning, trimming and thread cleaning
- Final inspection and packing
- Material handling and cutting-room support
Count each cluster separately and record the number of stations that are occupied, the number idle, and the number broken. The third category is the most informative number on the floor and the one least often disclosed. A factory with 120 sewing stations, 14 idle and 6 awaiting repair has an effective sewing base of 100, not 120.
Two further adjustments matter.
Indirect Labour
Cutting-room staff, material handlers, mechanics and quality inspectors support output but do not produce it directly. A ratio of direct to indirect labour above roughly 8:1 is healthy for a mid-sized bag factory; a ratio near 4:1 suggests either heavy quality overhead or a bloated support structure, and in the second case the quoted capacity is being carried by fewer producers than the headcount implies.
Skill Distribution
Not every operator can run every operation. A floor of 100 operators where 12 can execute the critical topstitch operation has a critical capacity of 12, not 100. Count stations by skill level for the two or three operations that determine quality, and treat the lowest number as the practical ceiling for that operation.
| Cluster | Stations counted | Occupied | Idle | Under repair | Effective |
|---|---|---|---|---|---|
| Cutting | 18 | 16 | 2 | 0 | 16 |
| Skiving | 22 | 19 | 1 | 2 | 19 |
| Edge paint | 14 | 12 | 0 | 2 | 12 |
| Sewing (all types) | 120 | 106 | 8 | 6 | 106 |
| Hardware | 16 | 14 | 2 | 0 | 14 |
| Inspection | 10 | 9 | 1 | 0 | 9 |
The pattern in that table is typical and diagnostically useful: the bottlenecks are almost never in sewing, because sewing is where factories invest. They sit upstream in skiving and edge work, where stations are expensive, skilled and few.
Takt Time and the Rhythm of a Line
Takt time is the pace a line must hold to meet demand: available production time divided by required output. For a line working 9.5 paid hours with 45 minutes of breaks and 30 minutes of meetings and cleaning, available time is 8.25 hours, or 495 minutes. To produce 480 pieces, takt time is 1.03 minutes per piece.
Takt time is a demand-side figure, not a capability figure. Its value in capacity assessment is that it forces the conversation onto balance: if the line's cycle time at the bottleneck exceeds takt, the line cannot meet the requirement no matter how many stations exist downstream.
Ask the factory to walk you through a balance calculation for a representative product. The calculation has five steps:
- Break the product into operations with standard times from an actual time study.
- Sum the operation times to obtain total work content.
- Divide total work content by the number of operators in the line to get average cycle time per operator.
- Identify operations whose individual time exceeds the average — these are the imbalance points.
- Adjust by combining or splitting operations, then recompute.
A line with 24 operators and 216 minutes of total work content averages 9 minutes per operator, which supports a piece every 9 minutes, or about 55 pieces per 495-minute day. If the edge-paint operation alone takes 14 minutes and can only be performed by four skilled operators, the line cannot reach 55 pieces; the true constraint is 4 operators × 495 minutes ÷ 14 minutes, or roughly 141 pieces — comfortable at 55, fatal at 200.
Presenting this calculation to a factory is one of the fastest ways to establish whether capacity claims are grounded. A factory that can produce the operation breakdown and the operator allocation is managing capacity. A factory that answers with a monthly total is quoting.
Finding the Bottleneck
Every line has one operation that sets the pace. Capacity assessment is, in practice, bottleneck identification, and the bottleneck is usually visible without instrumentation: it is where work in progress accumulates.
Look for the pile of cut panels, the trolley of unskived edges, or the rack of bag bodies waiting for hardware. The pile location is the constraint. Confirm it with time observation rather than inference — a stopwatch on one operator at that station for ten cycles gives a reliable cycle time.
Work through the arithmetic for a structured shoulder bag, assuming a single-shift line of 495 available minutes:
| Operation | Standard time (min) | Skilled operators | Theoretical capacity/day | Practical capacity/day |
|---|---|---|---|---|
| Cutting | 3.2 | 6 | 928 | 780 |
| Skiving | 4.1 | 5 | 604 | 480 |
| Edge paint (2 coats) | 6.8 | 4 | 291 | 250 |
| Main assembly sewing | 22.5 | 18 | 396 | 340 |
| Hardware setting | 2.9 | 5 | 854 | 700 |
| Final inspection | 5.5 | 5 | 450 | 400 |
The practical capacity of the line is 250 pieces per day, set by edge painting. Everything else has headroom, and the sewing floor — the part of the factory most likely to be shown to visitors — is sitting at 340 while the line delivers 250. A buyer told "we can do 400 a day" is being quoted the sewing capability, not the line capability.
There are four legitimate responses to a bottleneck, and each has a cost that the assessment should surface:
- Add station capacity. More edge-paint stations or a second shift on that operation. Fastest, most expensive.
- Offload the operation. Subcontract edge painting, which introduces an outsourcing dependency (see below) and a quality variable.
- Redesign the product. Change the edge construction to reduce paint passes — an engineering solution that requires the buyer's agreement.
- Extend the calendar. Run edge painting on weekends while assembly rests. Effective only if the operation is truly decoupled, which requires buffer stock and handling discipline.
A factory that cannot articulate which of these it will use for your product, and at what cost, has not planned your order. It has accepted it.
Efficiency, Attendance and the Realistic Hour
Theoretical capacity assumes every operator works every available minute at standard pace. Real factories do not. Three deductions must be applied, and the assessment should test each.
Line Efficiency
Efficiency is measured as earned standard minutes divided by attended minutes. Mature bag lines running stable products typically achieve 70 to 82 percent; new products in their first weeks run 55 to 65 percent and climb. A factory claiming 95 percent efficiency on a first order is either measuring something else or not measuring.
Attendance and Turnover
Absenteeism in labour-intensive regions runs 3 to 8 percent on ordinary days and rises sharply around holidays. Turnover matters more than absenteeism for capacity because it resets the efficiency curve: a line that loses fifteen percent of its operators each quarter never fully reaches mature efficiency on complex products.
Rework and Re-inspection
Rework consumes capacity invisibly. A five percent defect rate that requires full re-inspection adds inspection minutes and often re-sewing minutes, and the effect compounds at the bottleneck.
Applying these factors produces the only number worth planning against:
Effective daily output = (available minutes ÷ standard minutes per piece) × line efficiency × attendance factor × (1 − rework factor)
For the structured bag above, with 250 practical pieces at the bottleneck, 0.78 efficiency, 0.94 attendance and 0.05 rework, effective output is 250 × 0.78 × 0.94 × 0.95, or about 174 pieces per day. Against a stated sewing capacity of 400, this is the figure that should anchor a delivery schedule.
| Assumption | Optimistic claim | Measured reality | Effect on 250-piece ceiling |
|---|---|---|---|
| Line efficiency | 95% | 78% | 195 pieces |
| Attendance | 100% | 94% | 183 pieces |
| Rework | 0% | 5% | 174 pieces |
| Working days | 30 | 26 | Monthly output falls by 13% |
None of these deductions is large on its own. Together they remove roughly thirty percent of the number a buyer was originally given, which is precisely the gap that appears as a delay in the third month.
Peak Season Occupancy and Calendar Loading
Capacity is a function of time, and the only meaningful question is capacity in the window you need. A factory can be simultaneously capable of 30,000 pieces a month and unable to deliver 6,000 in November.
The tool for resolving this is a load-versus-capacity calendar, by line, by week, for at least the next three months. Ask for it in writing. What you are looking for is not the total but the shape:
- Which weeks are already above 90 percent committed?
- Which customers occupy the peak, and are they historic or new?
- Where are the empty weeks, and are they empty because the factory is free or because it cannot sell?
- Does the committed load assume overtime that has not yet been agreed with the workforce?
A representative loading sheet, anonymised, looks like this:
| Week | Available line-days | Committed line-days | Occupancy | Note |
|---|---|---|---|---|
| W45 | 120 | 78 | 65% | Normal |
| W46 | 120 | 96 | 80% | Two orders ramping |
| W47 | 120 | 114 | 95% | Peak; overtime assumed |
| W48 | 120 | 118 | 98% | No buffer for rework |
| W49 | 120 | 110 | 92% | Shipping week |
| W50 | 120 | 84 | 70% | Post-peak release |
| W51 | 120 | 62 | 52% | Holiday reduction |
Two things become visible in a table this simple. First, W47 and W48 have no rework buffer; a defect problem in those weeks becomes a delay. Second, W51 is nominally free but falls in a holiday period, so its 52 percent occupancy is worth less than the number suggests. Buyers who book into that week discover that the factory meant calendar days, not working days.
Occupancy above 85 percent is the practical ceiling for reliable delivery of new work, because new work consumes more capacity than mature work: it runs at lower efficiency, generates more questions, and requires more supervision. A factory at 95 percent occupancy that accepts a new buyer's first order is either displacing someone or planning to disappoint someone. It is worth asking which.
Also ask about the booking rule: well-run factories hold reservations against deposits and release them on a published schedule, while a factory with no rule runs first-come, and your slot is only as secure as the next customer's urgency.
Outsourcing Ratios and What They Hide
Most bag factories outsource some portion of their work. Common outsourced elements are edge painting, embroidery, printing, metal plating, carton production and, in peak periods, whole sewing sub-assemblies. Outsourcing is legitimate. Undisclosed outsourcing is a capacity risk, because it moves output outside the factory's control while leaving the commitment inside it.
Assess the outsourcing ratio in three dimensions.
By Value
What proportion of the order's production value leaves the factory? A factory that outsources edge painting on a product where edge work is fifteen percent of labour content is outsourcing fifteen percent of its own capacity. A factory that outsources whole sewing assemblies may be outsourcing fifty percent.
By Control
Does the factory own the sub-supplier's tooling? Does it station its own quality inspector there? Is the sub-supplier exclusive, shared, or opportunistic? Shared sub-suppliers are the first to fail in a peak, because everyone's orders arrive at once.
By Disclosure
Is the outsourcing declared in the quotation and named in the quality agreement? A factory willing to name its sub-suppliers and accept inspection at their premises is managing the dependency. A factory that describes all production as in-house and is later found to be brokering is not.
Verification is straightforward: ask to visit the sub-supplier for any operation above a threshold you set, and ask for the sub-supplier's monthly capacity figure and current load. If both answers arrive without friction, the dependency is being managed. If either meets resistance, treat the outsource ratio as higher than stated.
Material and Component Constraints on Capacity
Labour capacity is the visible constraint. Material availability is the one that stops lines, and it is frequently omitted from capacity assessments because it does not belong to the factory at all.
For a bag, four material categories gate production:
- Leather hides or coated fabric rolls — lead times of four to eight weeks, longer for custom colours and drum-dyed lots.
- Hardware — three to six weeks for stock items, eight to twelve for custom tooling.
- Zippers — two to four weeks for standard tape, longer for custom pulls or pantone-matched tape.
- Linings and interlinings — usually fast, occasionally the actual constraint when a specific weight or hand is required.
Assess whether the factory holds material safety stock and how it is allocated. A factory with two weeks of its three highest-use linings on the shelf can absorb a supplier delay. A factory that buys material against each order transfers every upstream delay directly into your schedule.
Ask the question in a way that produces a number: "For this product, what is the longest lead-time material, and what is your current stock position against it?" The answer reveals whether capacity planning includes material or assumes it away.
There is also a matching constraint that is specific to leather work. Hides arrive with natural variation in thickness, temper and shade. A line calibrated for one lot will slow when the next lot arrives, because operators adjust tension and feed, and because more panels are rejected at cutting. Factories that cut leather for bags typically plan a yield of 75 to 85 percent of the hide area and a cutting-room capacity that matches the sewing floor's requirement at that yield. A capacity claim that assumes 95 percent yield will not survive the second lot.
Sampling, Development and Pre-Production Load
New orders do not begin at bulk. They begin with sampling, and sampling consumes the same skilled people who would otherwise produce. This is the most consistently underestimated capacity cost in the buyer's plan.
A development cycle for a structured bag typically requires a first prototype, two or three revised samples, a pre-production sample made from production materials on a production line, and then the pre-production meeting. In factory terms that is 40 to 90 skilled hours consumed before a single sellable piece exists, concentrated in the sample room and in the pattern maker's time.
Sample rooms are small. A ten-person sample room cannot process more than three or four new developments a month, and that limit binds even when the sewing floor is empty. When a buyer places a first order in a busy season, the realistic question is not "do you have line time" but "do you have sample-room time in the next three weeks". Those are different resources with different calendars, and only one of them appears in the quotation.
The pre-production load also deserves explicit scheduling. A pilot run consumes line time at low efficiency — often 40 to 60 percent of mature output — plus supervision, quality attention and material handling, so a pilot of 300 pieces may occupy capacity equivalent to 500 or 600 pieces of mature production. Factories that quote the pilot at bulk rates understate what it will cost the schedule.
Verifying the Claim: The Walk-Through Assessment
Capacity verification is a physical exercise. Documents help, but the floor is the evidence, and a two-hour walk can establish more than a month of correspondence.
Arrive without warning if possible; a factory that needs a week's notice is telling you what the visit will show either way. If unannounced is not practical, insist that the walk includes the material store, the cutting room and the sub-assembly area — places that cannot be staged as quickly as an assembly line.
| What to observe | What it proves | What it disproves |
|---|---|---|
| Station count and occupancy | Real direct labour base | Headcount claims |
| WIP pile location | The actual bottleneck | Sewing-capacity claims |
| Time study on one station | Cycle time versus quoted standard | Efficiency assumptions |
| Material store depth | Buffer against supply delay | Just-in-time claims |
| Sample room load | Development bandwidth | "We can start next week" |
| Repair bench volume | Hidden rework load | First-pass yield claims |
| Packing area backlog | Post-sewing constraint | Line-balanced claims |
| Overtime board or shift log | Calendar realism | Working-day assumptions |
Four observations carry disproportionate weight.
The Work-in-Progress Profile
Walk the line from cutting to packing and note where buffers sit. A balanced line has small, even buffers. A line with one large pile has one bottleneck; a line with piles at several points has a scheduling problem rather than a capacity problem, which is often worse to fix.
The Repair Bench
Every factory has one. Count the pieces on it and ask how long they have been there. A bench with fifty pieces awaiting rework on a day when the line produced 250 tells you the first-pass yield is far below the claim.
The Idle Stations
Idle stations are either a hiring gap or a demand gap. Ask which. The answer is a direct read on whether the factory has capacity to sell or is quietly shrinking.
The Clock
Time one operation yourself, at the station with the largest queue, for ten cycles. Compare with the standard time used in the capacity calculation. A discrepancy above fifteen percent means the capacity model is built on numbers that were negotiated rather than measured.
Documents Worth Asking For
Documents do not prove capacity, but their absence is informative and their content supports the arithmetic.
- Capacity statement by line, naming the reference product, standard minutes, shift pattern and working days used to derive the monthly figure.
- Standard minute sheet for the product being quoted, by operation.
- Load-versus-capacity calendar for the next twelve weeks, by line.
- Outsourcing register, naming sub-suppliers, operations, and their capacity.
- Shift and overtime schedule, including planned weekend work, and an equipment list that reconciles the cutting and skiving base against the sewing base.
- Organisation chart for production, showing line supervisors, quality inspectors and mechanics per line.
- Recent monthly output by line for the last six months, which is the single most useful document in the set because it is historical rather than aspirational.
Historical output deserves more scrutiny than forward-looking capacity, because it shows seasonality, trend and volatility. A factory producing 22,000, 24,000, 31,000, 19,000, 23,000 and 25,000 pieces across six months has an average of 24,000 and a planning figure closer to 22,000: the peak is not repeatable, and the trough is what you experience if your order lands in it. Ask which months ran overtime — the gap between peak and median is overtime capacity, and it is already spent.
Trial Orders and Capacity Probes
A trial order is a capacity test disguised as a commercial transaction, and it should be designed as one.
The standard trial is 200 to 500 pieces. Design it to probe the constraint rather than to be easy: include the operation you believe is the bottleneck, use production materials rather than sample-room stock, and specify the packaging. A trial that avoids the difficult operations measures only the easy ones.
Four measurements should come out of the trial, recorded by both sides:
- Pieces per line-day achieved, against the pre-agreed forecast.
- First-pass yield at final inspection, by defect category.
- Actual cycle time at the bottleneck, compared with the standard used in planning.
- Elapsed days from material issue to packing, including any waiting.
How the factory recovers is as informative as the numbers: a factory that adds a shift at its own cost to rescue a trial controls its capacity, while one that blames material or the buyer does not.
Scale the trial result with discipline. If the trial achieved 180 pieces per day where planning assumed 250, the bulk forecast should be rebuilt at 180, not at 250 with a promise of improvement. Improvement curves are real — typically five to eight percent per week on a stable product — but they apply to efficiency, not to a structural bottleneck, and a trial that is bottleneck-limited will not improve by repetition.
Red Flags in Capacity Conversations
Certain answers recur in assessments that later go wrong. They are not proof of dishonesty; they are indicators that the capacity model is not being managed.
- A capacity figure with no reference product. The number cannot be verified because it does not describe anything.
- Refusal to provide line-level load. Total occupancy is offered instead. Aggregate occupancy hides the fact that the one line capable of your product is full.
- "We will add a shift." Adding a shift requires operators, and operators are the scarce input. A promise of a second shift without a named recruiter, a training plan and a start date is a promise to hire, not a capacity plan.
- Efficiency claims above 90 percent on new products. Physically unlikely; indicates the metric is not earned minutes over attended minutes.
- Vagueness about sub-suppliers. "We do everything here" is rarely true and never verifiable.
- Capacity that changes when you ask twice. Ask the same question on two occasions, weeks apart, and compare. Consistency is evidence of a system; variation is evidence of a conversation.
The last item is a technique worth institutionalising: record the capacity figure, the reference product and the date in the first meeting, then ask again during the trial. Factories that manage capacity give the same answer, adjusted for the load that arrived in between. Factories that quote give whatever number the moment requires.
Structuring a Capacity Agreement
Capacity that has been measured should then be written down, because the schedule depends on it and the schedule is what the buyer is actually purchasing.
A workable capacity agreement contains five elements.
A Defined Unit and Reference Product
Monthly output of the specific product family, expressed in both pieces and standard minutes, with the operation breakdown attached as an annex.
A Booking Mechanism
Line-days reserved per month, the deposit or forecast that secures them, and the release rule if the forecast is not confirmed by a stated date.
A Load Disclosure Obligation
The factory reports occupancy for the booked lines monthly; the buyer is entitled to know whether the line is at 60 or 95 percent, because that determines the rework buffer and the real delivery date.
A Change Protocol
How much notice is required for quantity changes, and what happens to capacity when a forecast is cut. Factories absorb cuts badly because capacity released late cannot be resold; a protocol that prices late cuts honestly is better for both sides than one that pretends flexibility.
An Escalation Path with Dates
What happens on day three, day seven and day fourteen of a shortfall, and who decides whether to add a shift, offload an operation or renegotiate the ship date.
| Element | Minimum acceptable form | Strong form |
|---|---|---|
| Unit | Pieces per month, reference product named | Pieces plus standard minutes, operation annex |
| Booking | Forecast acknowledged in writing | Line-days reserved against deposit, release rule stated |
| Disclosure | Occupancy reported quarterly | Monthly line-level occupancy with rework buffer disclosed |
| Change | 30 days notice for quantity change | Tiered notice with priced cut charges |
| Escalation | Weekly call | Dated escalation ladder with named decision-makers |
It does not need to be a contract annex: a two-page schedule appendix signed by both production heads is usually more effective than contract language, because it is read by the people who schedule the line.
Capacity for Growth: What Headroom Costs
The final question a buyer should ask is not "how much can you make" but "how much can you make if we double".
Growth capacity is a different asset from current capacity. It requires hiring ahead of demand, training on the specific product, additional tooling to break bottlenecks, and floor space that is currently either empty or leased to someone else. Each has a cost and a lead time.
- Hiring and training: six to ten weeks before a new operator reaches sixty percent of standard on a complex product. Capacity added by hiring is not available next month.
- Tooling duplication: two to four weeks for jigs, templates and dies. This is the cheapest way to break a station bottleneck and the least often planned.
- Sub-supplier qualification: four to eight weeks to qualify a new edge-painting or hardware supplier to the required standard.
- Floor space: an existing building can be reconfigured in weeks; a new one takes a year.
A factory that can describe its growth path in these terms — with dates and costs — is one that has thought about capacity as a system. A factory that answers "no problem, we can expand" without a plan is answering a question about optimism rather than about production.
For the buyer, the conclusion is that headroom should be contracted rather than assumed. If a programme is expected to grow by fifty percent within two quarters, the capacity agreement should include a growth clause with a trigger, a quantity band and a lead time, agreed while the factory is still competing for the business.
Frequently Asked Questions
Q: What single question best reveals real capacity?
A: "What is the standard minute value of this product, and what is the cycle time at your bottleneck operation?" A factory that can answer both is measuring capacity. A factory that answers with a monthly total is quoting.
Q: How many pieces per day should a bag factory deliver per sewing station?
A: For structured bags with twelve to twenty-five minutes of work content, four to eight pieces per station per day is a realistic range at mature efficiency. Figures far above that imply simple products, heavy subcontracting or a different counting basis.
Q: Is a factory at 95 percent occupancy a bad choice?
A: Not necessarily, but it changes the terms. At that load there is no rework buffer, so the delivery date should be padded rather than trusted, and the buyer should require weekly line-level status. A 70 percent factory with a worse reputation may deliver more reliably.
Q: How long does it take to verify capacity properly?
A: One floor visit of two to four hours, a document request that takes the factory a week to assemble, and a trial order of 200 to 500 pieces. The trial is the only step that produces data the factory cannot curate.
Q: What if the factory refuses a capacity assessment?
A: Treat refusal as a finding. Some factories refuse because their numbers are weak; others refuse because they have never been asked. The second group will usually comply once the purpose is explained as scheduling rather than auditing, and the first will not.
Q: Can capacity be increased by running overtime?
A: Overtime extends available minutes, not stations. It helps when the constraint is labour hours and hurts when the constraint is a four-station edge-paint operation that already runs two shifts. Overtime also degrades efficiency after roughly ten hours, so its marginal output is lower than the arithmetic suggests.
Q: What is a reasonable rework buffer in a capacity plan?
A: Ten to fifteen percent of committed capacity is workable for a mature product. Below five percent, a single defect cluster becomes a shipment delay. Factories running above 90 percent occupancy rarely hold this buffer, which is why peak-season delivery is unreliable even at capable suppliers.
What to Do Before the Next Quotation Arrives
Capacity assessment is not a distrust exercise. It is the process by which a schedule becomes an engineering document instead of a hope, and it benefits the factory as much as the buyer, because a factory that knows its real constraint can decline work it cannot run instead of accepting it and failing.
The practical sequence is short. Ask for the standard minute value and the bottleneck cycle time. Count stations and note the work-in-progress piles. Request twelve weeks of line-level loading and six months of line-level output. Walk the material store and the repair bench. Run a trial of 300 pieces that includes the difficult operation, and measure four things. Then write the resulting capacity into the booking terms, with a disclosure obligation and an escalation ladder.
Do that, and the number you plan against will be the number the floor produces. Skip it, and the difference will be discovered by a customer, in a peak season, at the point where nothing can be recovered.
A bag factory that can show you its bottleneck, its load calendar and its repair bench is not exposing weakness. It is demonstrating that it knows where its capacity ends — which is the only reliable basis on which a buyer can plan a programme that grows.