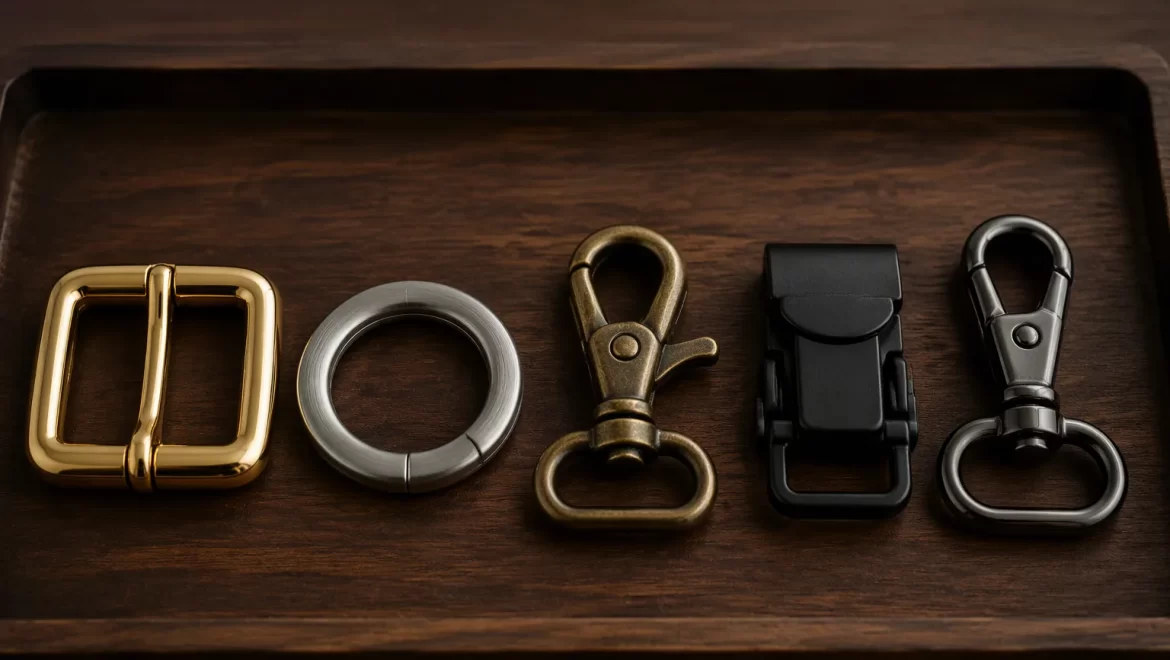
Hardware Finishes Compared: Polished, Brushed, Antique and PVD
- What "Finish" Means on Bag Hardware
- The Main Finishes Compared
- How Each Finish Wears
- PVD: The Durable Option
- Plating Options and Their Limits
- Corrosion and Perspiration Testing
- Matching Finish to the Bag
- Cost Drivers
- Specifying Hardware Finish
- Common Defects in Hardware Finishing
- Common Misconceptions
- Hardware Sourcing and Supplier Coordination
- Repair, Replacement and Long-Term Service
- How Finish Choice Affects Brand Perception
- Storage, Handling and Transit Protection
- FAQ
Hardware is the smallest part of a leather bag and the one that fails most visibly. A buckle that loses its plating, a zipper pull that turns dark, a ring that develops a green tinge after a humid summer: these small failures undermine the perceived quality of an otherwise well-made product.
Most of them trace back to the finish rather than to the shape or the design. Finish determines how the surface behaves against abrasion, moisture, salt and time, and it is specified far less carefully than it should be. Buyers routinely approve a finish from a photograph taken in studio lighting and discover, months into production, that the same finish behaves differently on a heavy-use handle ring than on a decorative plate.
This guide explains what "finish" actually describes in bag hardware, compares the main options (polished, brushed, antique, matte and PVD-coated, plus electroplated variants), explains how each wears and fails, covers corrosion and artificial perspiration testing, addresses how finish should be matched to leather and to wear points, outlines the cost drivers, and gives the specification and acceptance criteria that prevent disputes.
What "Finish" Means on Bag Hardware
The word covers three separate layers, and confusing them leads to specifications that cannot be met.
The Base Metal
Every component starts as a base material: zinc alloy, brass, stainless steel, aluminium or steel. The base determines strength, weight and, to a degree, how well a finish can be applied.
Zinc alloy is common because it casts complex shapes economically. Brass machines and casts well and takes plating readily. Stainless steel resists corrosion on its own, which changes the role of the finish from protection to appearance.
Plating Versus Coating
Plating deposits a metal layer onto the base through an electrochemical process. Coating applies a different material on top, which may be a lacquer, a paint or a vacuum-deposited film.
Plating becomes part of the component's surface; coatings sit above it. That distinction predicts how each behaves when worn or damaged.
Finish as the Final Surface
What the customer sees and touches is the final surface treatment: the polish level, the brush direction, the artificial patina, the matte texture or the coloured film. It is applied last and is the layer that determines first impressions and wear behaviour.
The Three Layers in Specification
| Layer | What it decides | Typical options |
|---|---|---|
| Base metal | Strength, weight, castability | Zinc alloy, brass, stainless steel |
| Intermediate | Corrosion protection, colour base | Nickel, brass, copper plating |
| Final finish | Appearance, wear behaviour | Polished, brushed, antique, matte, PVD |
The Main Finishes Compared
Each finish produces a distinct visual language and a distinct wear profile.
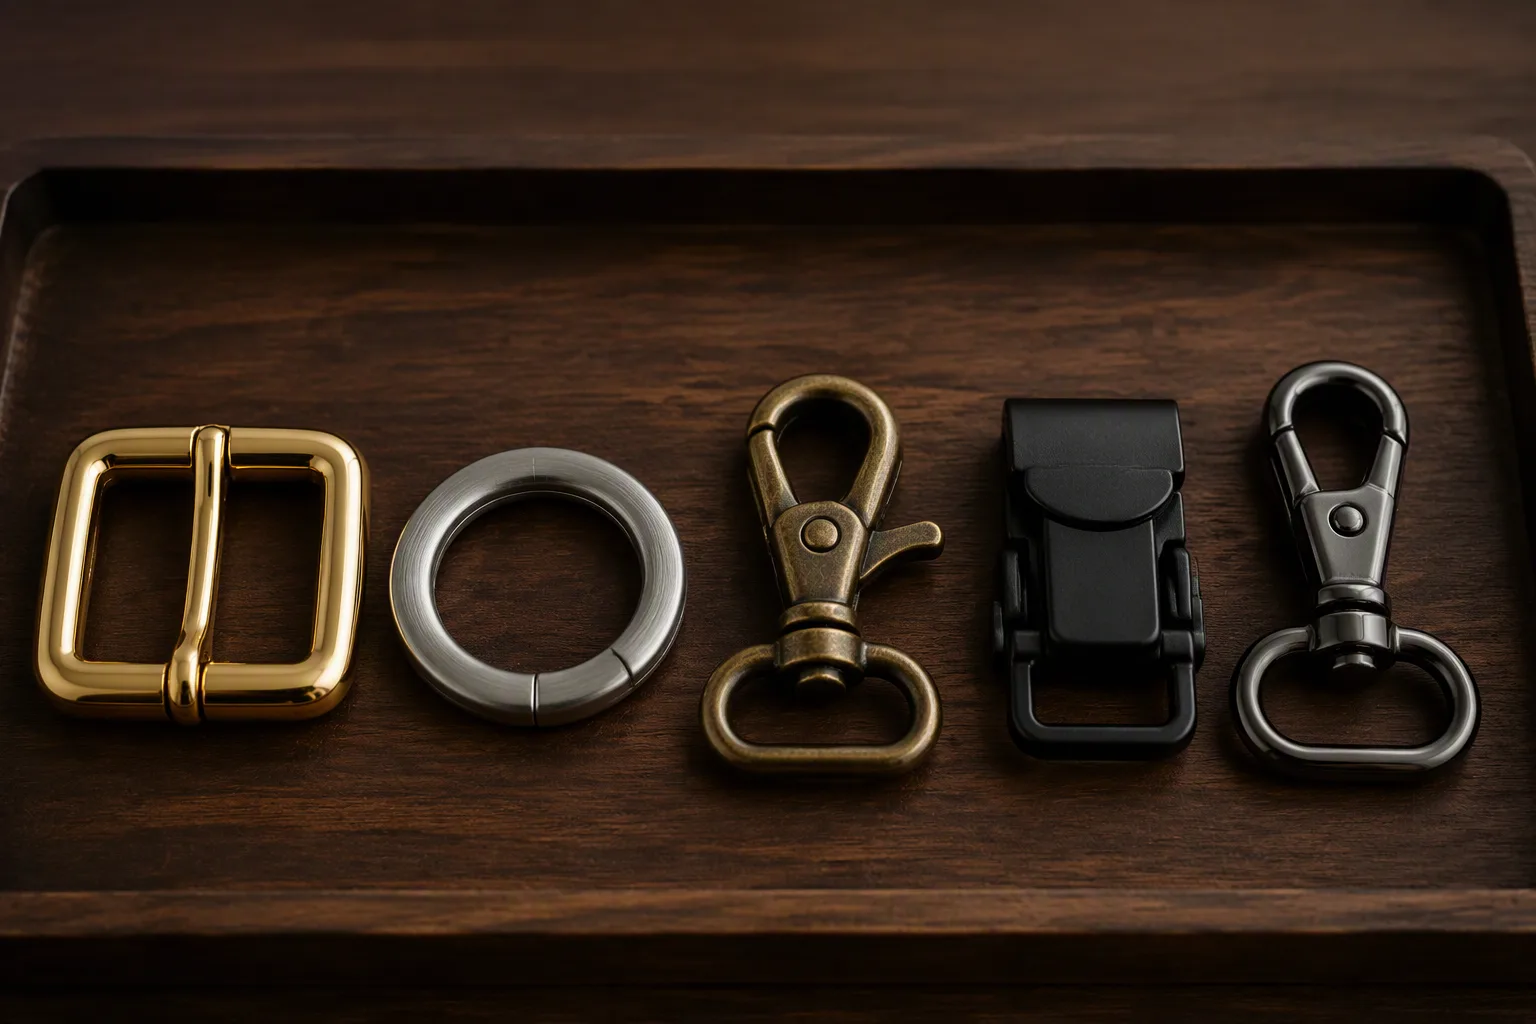
Polished and Bright
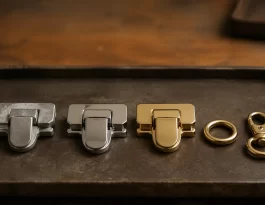
Polished hardware is buffed to a mirror surface. It reads as formal and premium and suits dress bags and structured designs.
Its weakness is visibility: polishing amplifies every scratch, and plated polished surfaces show wear as bright or dark spots where the plating thins.
Brushed and Satin
Brushed finishes are produced by abrading the surface in a consistent direction, leaving fine parallel lines. The result diffuses light and hides minor scratches far better than a polished surface.
Brushed finishes suit casual and daily-use bags, and they are more forgiving in production because small handling marks do not show.
Antique and Oxidised
Antique finishes darken the recesses of a component and highlight the raised areas, producing depth and an aged character. The effect is achieved through oxidation or chemical treatment during finishing.
Antique finishes hide wear well because the surface is already uneven in tone. They pair naturally with warm brown leather, and they have become a common default for heritage-style bags.
Matte and Pearl
Matte finishes scatter light and reduce reflection, giving a softer, more modern appearance. Pearl and satin-matte variants add a slight sheen without gloss.
Matte surfaces show fingerprints and oily marks more readily than brushed surfaces, and they can be difficult to clean uniformly once contamination sets in.
PVD-Coated
Physical vapour deposition applies a thin, hard film in a vacuum, producing colours that are difficult to achieve by plating and a surface significantly more resistant to abrasion and corrosion.
PVD is discussed in more detail below because its behaviour differs enough from plating to justify separate treatment.
Finish Comparison
| Finish | Appearance | Scratch visibility | Tarnish resistance | Relative cost | Typical use |
|---|---|---|---|---|---|
| Polished | Mirror gloss | High | Moderate | Baseline | Dress and structured bags |
| Brushed | Directional satin | Low | Moderate | Baseline | Daily-use bags |
| Antique | Darkened relief | Low | Moderate | Slightly higher | Heritage and casual |
| Matte | Soft, non-reflective | Moderate | Moderate | Baseline | Modern minimal designs |
| Pearl | Subtle sheen | Moderate | Moderate | Slightly higher | Fashion lines |
| PVD | Hard coloured film | Very low | High | Higher | Premium and heavy-use |
How Each Finish Wears
Finish failure follows a small number of mechanisms, and understanding them makes the choice of finish a deliberate decision rather than an aesthetic one.
Abrasion
Contact with hands, clothing, tables and bag contents removes material from the surface over time. Polished surfaces show abrasion as a loss of gloss; plated surfaces show it as exposure of the layer beneath.
Components that see constant friction, such as zipper pulls, handle rings and magnetic closures, wear fastest.
Corrosion
Moisture, salt from perspiration and airborne pollutants attack metal surfaces. Plated components corrode where the plating is thin, porous or damaged, producing pitting, discolouration or a green tinge on copper-bearing layers.
Coastal and humid markets stress hardware more than dry inland markets, and a finish that performs well in one may fail in the other.
Tarnish and Discolouration
Some metals darken as their surface chemistry changes. Brass and copper-based layers tarnish readily, and protective lacquers slow but do not stop the process. Once a lacquer is breached, tarnish can spread beneath it and appear as blotches.
Failure Modes by Finish
| Failure mode | How it appears | Most affected finishes |
|---|---|---|
| Abrasion wear | Gloss loss, exposed base metal | Polished, thin plating |
| Plating peel | Flaking, blistering at edges | Poorly prepared plating |
| Corrosion | Pitting, dark spots, green tinge | Thin or porous plating |
| Tarnish | Overall darkening | Brass and copper layers |
| Lacquer breakdown | Patchy discolouration | Lacquered bright finishes |
| Colour shift | Dulling, uneven tone | Matte and pearl finishes |
PVD: The Durable Option
PVD has moved from a specialist process to a mainstream option for bag hardware, and it solves problems that plating cannot.
How It Works
In a vacuum chamber, a source material is vaporised and deposited onto the component as a thin film, often with an intermediate layer beneath it. Because the film is deposited rather than electrochemically grown, it can be formed from materials that plating cannot apply.
The process produces a hard surface in colours such as black, gunmetal, gold-tone, rose-tone and bronze-tone without relying on a soft metal layer.
Where PVD Wins
PVD resists abrasion markedly better than plated surfaces, which matters on high-contact components. It also resists corrosion and perspiration better, extending the period before visible deterioration in humid conditions.
For heavy-use bags and for hardware that will be touched constantly, PVD often produces a better customer experience over the product's life than a brighter but softer finish.
Where PVD Has Limits
Colour matching is less flexible: the achieved tone varies with the substrate, the film thickness and the machine, so consistency between batches must be confirmed against an approved sample.
Cost is higher than standard plating, and reworking a rejected component is not straightforward. PVD also performs best on a smooth, well-prepared substrate, so the base metal and its preparation matter more, not less.
PVD Suitability
| Consideration | PVD performance |
|---|---|
| Abrasion resistance | High |
| Corrosion resistance | High |
| Perspiration resistance | High |
| Colour range | Good for dark and metallic tones |
| Colour consistency | Requires sample approval |
| Cost | Higher than plating |
| Best use | High-contact and heavy-use hardware |
Plating Options and Their Limits
Plating remains the most widely used approach, and its behaviour depends on preparation and thickness as much as on the metal used.
Common Plating Systems
Nickel plating provides a hard, bright base and is often used beneath other layers. Chrome gives a bright, hard surface. Brass and copper-based platings produce warm tones and serve as a base for antique finishes.
Where a warm gold tone is required, brass-based plating is common, though it tarnishes and is often protected by a lacquer.
Thickness and Quality
Plating quality depends on the thickness of the deposited layer, the uniformity of that thickness and the cleanliness of the substrate before plating. Thin plating on a poorly prepared surface fails at the edges and in recesses first, because deposition is least uniform there.
Specifying plating quality by thickness rather than by appearance is more reliable, and it should be verified on a sample rather than assumed.
Skin Contact Considerations
Hardware that contacts skin frequently, such as a shoulder strap ring or a closure on a wristlet, is subject to perspiration and repeated friction. Where nickel-bearing layers are involved, buyers with markets sensitive to nickel content should specify the surface layer accordingly, and confirm through testing that the released material stays within the limits that apply in that market.
Plating Comparison
| Plating system | Appearance | Hardness | Tarnish risk | Notes |
|---|---|---|---|---|
| Nickel | Bright, slightly warm | High | Low to moderate | Common base layer |
| Chrome | Bright, cool | Very high | Low | Hard, formal look |
| Brass | Warm gold tone | Moderate | High | Usually lacquered |
| Copper-based | Warm, antique base | Low | High | Base for antique finishes |
| Gold-tone | Warm, decorative | Moderate | Moderate | Thickness drives life |
Corrosion and Perspiration Testing
Testing turns finish selection from an opinion into a comparison, and it is the only reliable way to compare finishes across suppliers.
Salt Spray Testing
Components are exposed to a saline mist in a controlled chamber for a defined period, then inspected for corrosion. The test accelerates what would happen over a much longer period in a humid or coastal environment.
Results are expressed as the time before a defined degree of corrosion appears, so the meaningful comparison is between finishes tested under identical conditions.
Interpreting Results
A component that shows corrosion only in recesses and at edges performs better than one with widespread surface corrosion. Where results differ substantially between two suppliers using nominally the same finish, the cause is usually plating thickness or substrate preparation rather than the finish itself.
Artificial Perspiration Testing
Perspiration is more aggressive than plain moisture because of its salt content and acidity. Artificial perspiration tests expose hardware to a solution that mimics it, then assess discolouration and corrosion.
For bags worn against the body or carried by hand for long periods, artificial perspiration testing predicts customer experience better than salt spray alone.
Test Types and Their Reading
| Test | What it simulates | What to compare |
|---|---|---|
| Salt spray | Humid or coastal exposure | Time to defined corrosion |
| Artificial perspiration | Skin contact | Discolouration and corrosion |
| Abrasion test | Repeated friction | Coating loss, gloss change |
| Adhesion test | Plating bonding | Flaking at edges |
| Humidity test | Storage and transit | Tarnish and blistering |
Matching Finish to the Bag
Finish choice works best when the hardware, the leather and the use pattern are considered together.
Leather and Hardware Pairing
Warm brown leathers generally suit antique, brass-tone and bronze-tone hardware, where the tones reinforce each other. Cooler tones and black leathers pair well with polished chrome or gunmetal finishes.
Tone-on-tone combinations read as more considered than high-contrast pairings, while contrast draws attention to the hardware as a design feature.
Consistency Across a Range
A range using different hardware across products looks assembled rather than designed. Where several bag styles share a collection, agreeing on one or two finishes and applying them consistently strengthens the identity.
Finish consistency is easier to maintain than exact colour matching, because subtle colorant variation between batches is unavoidable and must be managed through an approved reference.
Durability by Wear Point
The component that is touched most should carry the most durable finish. A common mistake is specifying a polished decorative finish on every component, including those that will be in constant contact with hands.
Matching Guidance
| Wear point | Contact level | Suggested finish |
|---|---|---|
| Zipper pull | Very high | PVD or brushed plating |
| Handle ring | Very high | PVD or brushed plating |
| Closure plate | Moderate | Polished or pearl |
| Decorative stud | Low | Any, including antique |
| Strap adjuster | High | PVD or antique |
| Interior hardware | Low | Any |
Cost Drivers
Hardware cost is a combination of base material, casting or machining, finishing and quantity, and the finish is only one part of it.
Base Material and Forming
The base metal and the forming method set the floor for cost. A cast zinc alloy component costs less than a machined brass one, and the difference is a material and process difference rather than a finishing difference.
Finishing Cost
Finishing cost rises with the number of layers, the precision of the surface preparation and the process used. PVD adds a vacuum process; multiple plating layers add process steps; hand-applied antique effects add labour.
Order Quantity and Batch Plating
Plating and coating are batch processes, so low quantities carry proportionally higher setup cost, and small batches can produce more variation between runs. Where a design is expected to repeat, keeping the same finishing supplier and the same batch parameters reduces drift.
Cost Structure Overview
| Cost element | Share of total | Notes |
|---|---|---|
| Base material | Significant | Alloy choice sets the floor |
| Forming | Significant | Casting versus machining |
| Surface preparation | Moderate | Drives finish quality |
| Finishing process | Moderate to high | Layers and process type |
| Setup and minimums | Variable | Falls with quantity |
| Quality inspection | Low | Rises with testing scope |
Specifying Hardware Finish
Finish disputes usually arise from vague descriptions, and a short specification prevents most of them.
Descriptive Language and References
Describe the finish with both a named type and a physical reference: brushed, satin direction consistent, referenced to the approved sample. Words such as "gold" or "premium" have no shared meaning across suppliers.
Where colour is critical, provide a reference component and state which lighting conditions matter, since hardware appearance shifts between daylight, retail lighting and photography.
Acceptance Criteria
State what constitutes acceptable variation: colour consistency against the reference, absence of visible plating defects at edges, uniformity of brush direction, and the performance test the finish must pass.
Sample Approval
Approve the finish on a physical sample produced with production processes, and keep it as the reference for the life of the product. Photographs alone cannot carry a finish specification because lighting changes the appearance.
Specification Checklist
| Item | Must be specified |
|---|---|
| Base metal | Yes |
| Finish type | Yes |
| Reference sample | Yes |
| Colour tolerance | Yes |
| Surface uniformity | Yes |
| Performance test | Where durability matters |
| Batch consistency requirement | Yes |
Common Defects in Hardware Finishing
Defects appear either immediately or after use, and both categories belong in the inspection plan.
| Defect | Appearance | Cause | Prevention |
|---|---|---|---|
| Plating peel | Flaking at edges | Poor substrate preparation | Surface control before plating |
| Blistering | Raised spots | Contamination, trapped gas | Cleanliness, process control |
| Uneven colour | Patchiness | Inconsistent film thickness | Batch parameters, sample check |
| Brush direction mismatch | Inconsistent lines | Manual handling | Direction control, jigs |
| Tarnish bloom | Dark patches | Thin lacquer, porosity | Thicker protection, better plating |
| Corrosion pitting | Dark spots after use | Thin plating, aggressive exposure | Salt spray and perspiration testing |
| Sharp edges | Rubbing injury | Deburring omitted | Deburring and inspection |
Common Misconceptions
Several assumptions about hardware finishing lead buyers to the wrong choice.
"Stainless Steel Never Changes Colour"
Stainless steel resists corrosion well, but it still shows scratches, fingerprints and, in some grades and environments, surface staining. Its finish still matters.
"Antique Means Lower Quality"
Antique finishes are deliberate treatments that hide wear effectively. A well-executed antique finish on a sound base outperforms a thin bright plating that exposes the base metal within months.
"PVD Solves Everything"
PVD improves abrasion and corrosion resistance, but it constrains colour matching, costs more and depends on substrate quality. It is the right answer for high-contact components, not a universal default.
"Any Plating Will Do for a Decorative Part"
Even low-contact parts are seen up close. Thin plating on a decorative plate can fail through handling and packing alone, before the bag reaches a customer.
Hardware Sourcing and Supplier Coordination
Finish quality depends as much on the supplier as on the specification, and coordination is where consistency is protected.
Standard Components Versus Custom Development
Standard hardware from a catalogue carries lower cost and shorter lead time, and its finish options are already proven. Custom components allow exact proportions and a finish tuned to the design, but they add tooling, development time and the requirement to prove the finish on a new part.
Many ranges use a mix: custom components at visible focal points, standard components elsewhere, specified in the same finish family so the range reads as coherent.
Tooling and Reuse
Hardware tooling belongs to the buyer when it is paid for, and that should be recorded along with where it is stored and what happens if the relationship ends. Reusing existing tooling across products is one of the cheapest ways to extend a range.
Sample and Batch Consistency
Approve a physical finish sample and keep it as the reference for every subsequent batch. Ask the supplier to state which parameters they control to hold the finish, and to record the plating or coating specification alongside the order.
Where several batches will ship in one season, ask for a colour comparison photograph of each batch against the reference before shipment, so drift is caught before goods leave the factory.
Coordination Practice
| Item | What to agree |
|---|---|
| Finish reference | Physical approved sample |
| Process specification | Plating or coating type and thickness |
| Batch records | Parameters and lot references |
| Tooling | Ownership, storage, transfer |
| Inspection | Criteria and frequency |
| Escalation | Who decides on a colour variance |
Repair, Replacement and Long-Term Service
Hardware is replaceable in a way that leather rarely is, and designing for replacement extends the service life of the whole bag.
Designing for Replacement
A component held by screws or a removable pin can be replaced; one riveted into the panel usually cannot. Where a bag is positioned as long-life, choosing replaceable fastening benefits the customer and reduces the cost of warranty claims.
Spare Parts Strategy
Keeping a small stock of the components most likely to need replacement, such as zipper pulls and closures, allows a repair rather than a replacement product. The spare should match the original finish, which is another reason to keep the reference sample.
Serviceability and Finish
Where a component is expected to be replaced, its finish should be reproducible over time. Highly bespoke finishes that depend on a specific batch parameter are difficult to reproduce years later, whereas standard finishes are easier to source again.
Service Considerations
| Design choice | Effect on service life |
|---|---|
| Screwed or pinned attachments | Replacement possible |
| Riveted attachments | Replacement impractical |
| Standard finish | Reproducible in future |
| Bespoke finish | Harder to match later |
| Spares held by brand | Faster repair |
| Spares held by factory only | Dependent on supplier |
How Finish Choice Affects Brand Perception
Finish is one of the few product details a customer touches on every use, and consistency across a range communicates a level of control.
Touch Points and Expectations
The components a customer handles most, such as closures and zipper pulls, form the tactile impression of quality. Spending the durability budget on these parts produces more perceived value than applying an expensive finish evenly across every component.
Line Differentiation
Finish is an efficient way to differentiate product tiers within a range: the same bag silhouettes can be positioned differently through hardware finish alone, from polished bright to PVD in a dark tone, without changing the pattern or the leather.
Market Differences
Humidity, climate and cultural preference all affect how a finish is received. Hardware specified for a dry inland market may show corrosion early in a coastal one, and tones that read as premium in one market may read as antique or unfashionable in another.
Where a product ships to several markets, the safest approach is to specify a finish that withstands the harshest environment in the range rather than optimising for an average.
Perception Levers
| Lever | Effect |
|---|---|
| Finish on high-touch parts | Strongest tactile impression |
| Finish uniformity across range | Reads as designed, not assembled |
| Environmental suitability | Prevents early visible failure |
| Tier differentiation | Positions products without new patterns |
| Finish durability | Reduces visible aging complaints |
Storage, Handling and Transit Protection
A finish that leaves the finishing supplier in perfect condition can arrive at the customer marked, because the damage happens between finishing and packing.
Packaging After Finishing
Hardware is usually packed loosely in bulk after finishing, and movement inside the bag abrades it. Separating components, wrapping them individually or using compartmented trays prevents the small collisions that dull a bright finish or scratch a brushed one.
Where a finish is particularly soft, such as a bright polished surface or a lacquered bright finish, individual wrapping is worthwhile even though it adds handling cost.
Storage Conditions
Humidity and airborne sulphur compounds accelerate tarnish. Components should be stored in sealed packaging with a desiccant where the climate is humid, and away from rubber and certain plastics that release reactive compounds over time.
Storage duration matters too. Components held for months across a humid season may show tarnish even without being used, so stock rotation and shorter storage periods protect the finish.
Handling During Assembly
Assembly is where most handling damage occurs. Operators touching bright hardware with bare hands leave oils that show as fingerprints and can promote corrosion, and piling components into open bins causes edge damage.
Simple measures work: gloves or finger cots for bright finishes, shallow trays rather than deep bins, and assembly fixtures that avoid metal-to-metal contact.
Protection in Transit
Finished bags are usually wrapped, but hardware is often the point where wrapping is thinnest. Where a component protrudes, such as a buckle or a stud, additional padding at that point prevents pressure marks on the leather and abrasion on the hardware itself.
Protection Measures
| Stage | Risk | Measure |
|---|---|---|
| Bulk packing after finishing | Component-to-component abrasion | Compartmented trays or individual wrap |
| Warehousing | Tarnish, humidity damage | Sealed packaging with desiccant |
| Long storage | Slow tarnish and oxidation | Stock rotation, shorter holding |
| Assembly handling | Fingerprints, edge damage | Gloves, shallow trays, fixtures |
| Packing | Pressure marks, rubbing | Local padding at hardware points |
| Transit | Vibration and contact | Filled cartons, no movement in box |
FAQ
Which hardware finish lasts longest on a bag that is used daily?
A: PVD-coated and brushed plated finishes last longest on high-contact parts. Polished surfaces show scratches and plating wear earliest because they reveal every change in surface condition.
Is antique finish less durable than polished?
A: Antique finishes are usually more forgiving of wear because the surface tone is already uneven. Thin bright plating that exposes the base metal is more likely to look worn early than a well-executed antique treatment.
How do I specify a finish so the supplier understands it?
A: Use a named finish type plus a physical approved sample, and state the performance test required. Descriptive words alone, such as gold or premium, are interpreted differently by different suppliers.
What does salt spray testing actually tell me?
A: It accelerates corrosion in a humid or coastal environment and reports how long the finish resists a defined degree of corrosion. It is most useful for comparing finishes tested under identical conditions.
Why do some zipper pulls turn dark within a season?
A: Perspiration, friction and humidity attack the surface layer. Thin plating or a lacquer that has broken down allows tarnish or corrosion to develop, especially on components that are handled constantly.
Should every component use the same finish?
A: Consistency across a range usually reads as more deliberate than mixed finishes, but durability requirements differ by wear point. A common compromise is one finish family with a more durable variant on high-contact parts.
Is PVD worth the additional cost?
A: For components that are touched constantly, it usually is, because it holds its appearance longer. For low-contact decorative parts, the benefit is smaller and standard plating may be sufficient.
Can hardware colour be matched exactly between batches?
A: Exact colour matching is not realistic for plated or coated finishes. Manage it through an approved reference sample and a stated tolerance, and check each batch against the reference before shipment.
How do I test hardware for skin contact durability?
A: Use an artificial perspiration test, which simulates the salts and acidity of contact with skin, and assess discolouration rather than only structural corrosion.
What plating thickness should I ask for?
A: Specify thickness rather than appearance alone, and verify it on a sample. Thin plating on a poorly prepared substrate fails at edges and recesses first, regardless of how it looks new.
Why does brushed finish hide scratches better than polished?
A: Brushed surfaces scatter light along fine directional lines, so small marks blend into the texture. Polished surfaces reflect uniformly, which makes any interruption highly visible.
Can hardware be re-plated or repaired?
A: Some components can be re-plated, but it is rarely economical for small parts. Designing with replaceable attachments and holding spare components is usually the more practical repair route.
Does the base metal matter if the finish is good?
A: Yes. The substrate determines how well a finish adheres, how the component performs structurally and how it behaves if the finish is damaged. PVD in particular depends on a well-prepared base.
How many hardware finishes should a collection use?
A: One or two finishes across a collection is usually enough. Beyond that, the range begins to look assembled from different sources rather than designed as a group.
What should be checked on incoming hardware?
A: Finish against the reference sample, uniformity of brush direction or polish, absence of plating defects at edges, function of moving parts, and dimensional fit with the leather panels.
How do I prevent finish disputes later in production?
A: Approve a physical sample, record the process specification and tolerance in the purchase order, and require batch comparison photographs before shipment rather than relying on appearance after arrival.
Ready to specify hardware that still looks right after a year of use? Share your bag design, target market and the components you are considering, and we will help you match finish to wear point: PVD and brushed plating where hands and friction do the most damage, antique and polished finishes where appearance leads, and performance testing that turns finish selection into a documented decision.