Suede and Nubuck in Bag Making: Handling, Strength and Care
- What Suede and Nubuck Are
- Nap Direction and Its Consequences
- Cutting and Handling
- Reinforcement and Construction
- Lining and Interior Treatment
- Durability and Wear
- Water, Stain and Cleaning Considerations
- Quality Control for Suede and Nubuck
- Specifying Suede and Nubuck
- Cost Considerations
- Common Misconceptions About Nap Leathers
- Working With Nap Materials in Sampling
- Nap Materials by Bag Category
- Packaging, Storage and Retail Handling
- Sourcing Nap Materials From Suppliers
- FAQ
Suede and nubuck give a bag a softness that smooth leather cannot reproduce, and they create a set of production problems that smooth leather never presents. A workshop that handles chrome-tanned cowhide competently can still ruin a suede order through contamination, wrong nap direction or edge treatment that was specified for grain leather.
The difficulties are predictable. Suede and nubuck are defined by a raised fibre surface, and that surface dictates how the material must be cut, handled, reinforced, sewn and finished. It also determines how the finished bag will age, what stains will do to it, and how much of the material's strength can actually be used in a load-bearing panel.
This guide covers the definitions that buyers and factories need to agree on, why nap direction matters more than most specifications acknowledge, how suede and nubuck behave at each production step, where reinforcement is required, how linings and edges should be handled, what durability and staining look like in practice, how quality is inspected, and how to write a specification that a factory can execute without guesswork.
What Suede and Nubuck Are
The two terms are used loosely in the trade, and the difference matters because it determines strength, appearance and cost.
Suede
Suede is produced by abrading the flesh side of a hide (or the surface of a split) to raise a fine, velvety nap. Because the flesh side is used, suede can be made from a split layer, which makes it accessible at lower cost and in larger volumes.
The nap on suede is soft and short. It marks easily, absorbs liquids readily and stretches more than the grain side of the same hide.
Nubuck
Nubuck is produced by lightly abrading the grain side of a full-grain hide. The result is a fine nap on what remains a strong, intact grain layer, which is why nubuck generally outperforms suede in tensile strength and shape retention.
Nubuck has a slightly denser, more compact nap than suede and typically carries a higher price because it uses the grain rather than a split.
Related Terms
Buyers will meet several adjacent terms. "Genuine suede" usually means a split-based suede. "Nubuck split" or "sueded split" refers to a split whose flesh side has been buffed. "Napa" describes a soft, smooth finish and is not a nap material at all.
Two-way stretch suede and bonded suede also appear; the first refers to elastic behaviour, the second to a reconstituted material, and both behave differently from a natural suede in production.
Type Comparison
| Type | Source layer | Nap feel | Tensile strength | Relative cost |
|---|---|---|---|---|
| Suede | Flesh side or split | Soft, short | Moderate | Lower |
| Nubuck | Grain side, buffed | Dense, fine | Higher | Higher |
| Sueded split | Split, flesh side buffed | Soft | Lower | Lower |
| Bonded suede | Reconstituted fibres | Uniform | Low | Lowest |
| Napa | Smooth, no nap | None | Higher | Varies |
Nap Direction and Its Consequences
Nap is the single most consequential characteristic of a nap material, and it is the one most often left unspecified.
With the Nap and Against It
Brushing the surface in one direction produces a lighter, smoother appearance; brushing against it produces a darker, rougher appearance. On a finished bag, light falling from different angles can make identical panels look as though they were cut from different hides.
The effect is not subtle. A bag assembled from panels cut in mixed directions can show visible tonal blocks that no amount of finishing will remove.
Consistency Across Every Cut Piece
The production rule is that all panels of the same bag, and ideally all bags within a production run, must be cut in the same nap direction. This includes panels that will not sit adjacent to each other, because lighting changes as the bag is handled.
Factories mark the nap direction on the pattern and record it on the cutting instruction sheet. Where a design requires a deliberate contrast, such as a panel laid against the nap for effect, that must be specified rather than left to the cutter.
Consequences for Material Yield
Cutting everything in one direction removes the freedom to rotate patterns to fit around defects, which reduces yield compared with a material where orientation does not matter.
The yield loss must be anticipated in costing. A pattern layout that fits comfortably on a hide when pieces can be rotated may need a larger hide or a higher consumption figure when nap direction is fixed.
Nap Handling in Practice
| Decision | Consequence |
|---|---|
| Nap direction specified | Consistent colour and light response |
| Nap direction unspecified | Visible tonal blocks |
| All pieces same direction | Higher consumption, better result |
| Mixed directions | Lower consumption, visible defects |
| Deliberate contrast specified | Design effect, requires sample approval |
Cutting and Handling
Nap materials punish careless handling more than grain leather, and the difference shows up from the first operation.
Cutting Behaviour
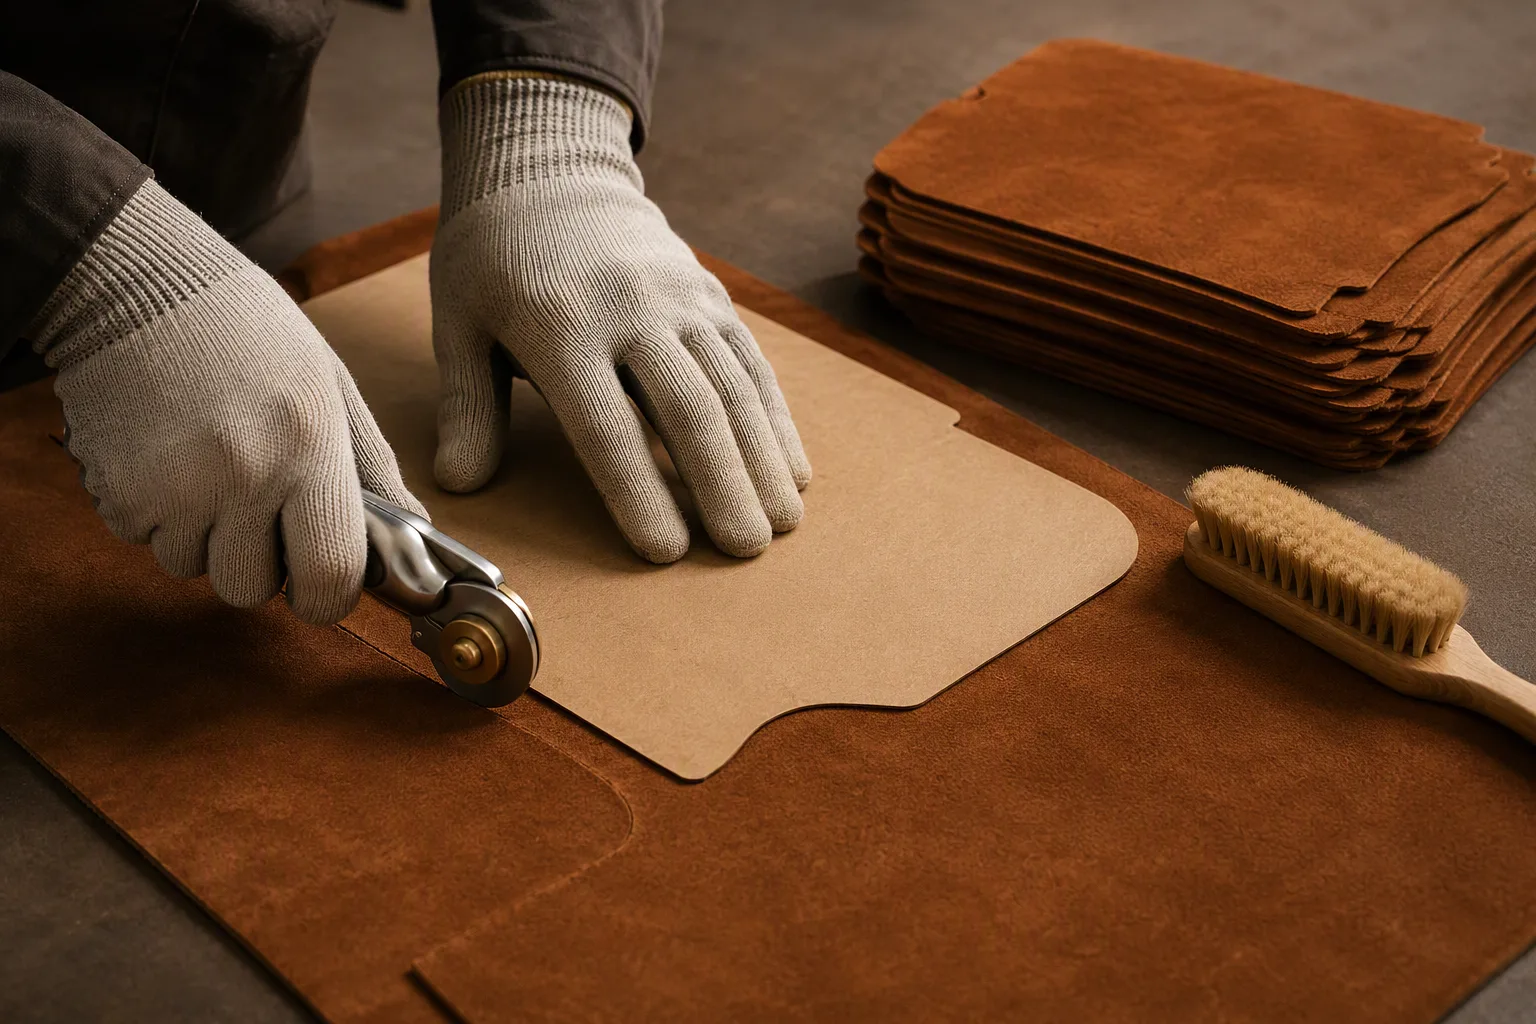
The raised surface creates friction against the blade and the cutting surface, so knife pressure and sharpness matter more. Blades dull faster on a nap material, and a dull blade drags fibres instead of severing them, producing a fuzzy or ragged cut edge.
Die cutting works, but the die must be sharp and the cutting pad clean. Water jet and laser cutting both need process adjustment, and laser cutting leaves a hardened, discoloured edge that is particularly visible on a nap surface.
Handling and Contamination
Suede and nubuck absorb oils from hands, and a fingerprint on a light-coloured nap may be permanent. Work in progress should be handled with gloves, kept off contaminated surfaces and covered between operations.
Workshops that handle both smooth and nap leathers should separate the two, because dust, adhesive residue and metal filings from other operations lodge in the nap and are difficult to remove.
Adhesives and Pressing
Adhesive applied to the back of a nap material can strike through to the surface, leaving a stiff, discoloured patch. Low-viscosity adhesives are the worst offenders, and nap materials benefit from higher-viscosity formulations applied thinly, with controlled drying before assembly.
Pressing is a separate risk: heat and pressure flatten the nap, and a flattened area on a suede panel reads as a permanent mark. Pressing should be done on the flesh side or with a protective cloth, at the lowest effective temperature.
Handling Risks
| Risk | Cause | Control |
|---|---|---|
| Ragged cut edge | Dull blade, dragging | Frequent blade changes |
| Fingerprint marks | Hand oils | Gloves on all handling |
| Adhesive strike-through | Low-viscosity glue | High-viscosity, thin application |
| Flattened nap | Heat and pressure | Reduced pressing, protective cloth |
| Cross contamination | Shared workshop | Separation from grain leather |
| Embedded dust | Workshop environment | Covered storage, clean benches |
Reinforcement and Construction
Nap materials need more structural help than their appearance suggests, and the construction strategy should be settled before sampling.
Strength and Reinforcement
Suede produced from a split has limited tensile strength and stretches under load, so panels that carry weight need backing. Nubuck is stronger because the grain layer is intact, but it still benefits from reinforcement where hardware attaches or where the panel will be pulled.
Reinforcement options include a bonded lining, a stitched-in reinforcement panel, or a laminated support layer applied during panel preparation. The choice affects the hand feel: a heavy reinforcement makes a suede bag feel stiff, which contradicts the reason for choosing the material.
Stitching Behaviour
Stitch lines sink into the nap, which can be an advantage for concealed joins but a problem where a decorative stitch is intended to be visible. Thread that reads clearly on grain leather may disappear on a nap surface.
Seam allowance also behaves differently. Two nap surfaces pressed together can slip during sewing, so the factory needs either a higher stitch density, a temporary adhesive, or a walking-foot machine that moves the layers together.
Edge Treatment
Edge paint, which works well on grain leather, sits badly on a nap edge and tends to wick into the fibres, producing a dark, uneven line. Folded edges or bound edges are the usual solutions, and they require the panel edges to be skived accurately.
Where a folded edge is used, the nap must be protected during folding, and the fold line should be set with controlled pressure to avoid a permanent flattened band.
Construction Options
| Construction element | Suede | Nubuck |
|---|---|---|
| Load-bearing panel | Reinforcement required | Reinforcement recommended |
| Hardware attachment | Backing patch essential | Backing patch recommended |
| Visible topstitch | Reads softly | Reads softly |
| Edge finishing | Folded or bound | Folded or bound |
| Adhesive use | High viscosity, thin | High viscosity, thin |
| Lining | Usually required | Commonly used |
Lining and Interior Treatment
A nap interior feels unfinished and wears poorly, so most suede and nubuck bags carry a lining.
Why Lining Matters
An unlined nap interior collects debris, transfers colour onto contents and stretches without restraint. A lining stabilises the panel, gives the bag a cleaner interior and protects the nap from abrasion caused by contents moving inside.
Lining Materials
Smooth textiles, microfibre and lightweight leather all work. The lining should be dimensionally stable, because a lining that stretches will pull the nap panel out of shape.
Where the bag will hold heavy contents, a lining bonded to the panel rather than floating free reduces distortion. The bond must be made with an adhesive that does not strike through, which returns the decision to the adhesive specification.
Joining Lining to Nap
Stitching a lining to a nap panel requires care at the seam line, because the nap can creep and create a wavy join. Factories commonly stitch the lining to the reinforcement layer rather than to the nap surface, keeping the nap free of perforations.
Interior Decisions
| Decision | Effect |
|---|---|
| Bonded lining | Stable, less distortion |
| Floating lining | Softer, more movement |
| Stitching into nap | Visible perforations |
| Stitching to reinforcement | Cleaner nap surface |
| Light lining | Retains softness |
| Heavy lining | Adds structure, reduces hand feel |
Durability and Wear
Nap materials age in ways that buyers should anticipate and either manage or communicate.
Nap Wear
Friction crushes or polishes the nap over time, producing areas that look shinier or darker than the surrounding surface. Common locations are the base, the handle area and any panel that rubs against the body.
Nubuck generally holds its surface longer than a split-based suede because the underlying layer is stronger, though the nap still changes with use.
Staining and Absorption
Nap surfaces absorb liquids, including rain, spilled drinks and oils from skin. A stain on a light suede can be very difficult to remove, and attempts to clean it can spread it.
Factory-applied protection reduces absorption but does not eliminate it, and buyers should treat protection as a performance improvement rather than a guarantee.
Shading and Tonal Change
Suede and nubuck change tone as the nap is brushed in different directions. This is normal behaviour, not a defect, but it means that two bags photographed in different lighting may appear to be different colours.
Communication matters here: retail partners who understand that the surface shifts in tone are less likely to file claims when it does.
Wear Risks
| Risk | Likely location | Mitigation |
|---|---|---|
| Nap polishing | Base, handle area | Protective treatment, reinforcement |
| Liquid staining | Any exposed panel | Water-repellent finish, care guidance |
| Oil absorption | Handle, closure | Handling discipline, treatment |
| Shading difference | All panels | Consistent nap direction |
| Edge fraying | Unfinished edges | Folded or bound edges |
| Colour transfer | Interior without lining | Lining specification |
Water, Stain and Cleaning Considerations
Protective treatments and clear care instructions reduce returns, and both are decisions made during production rather than after.
Water-Repellent Treatment
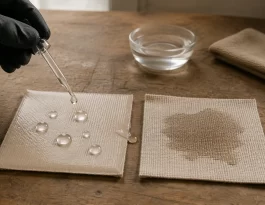
Fluorocarbon-free and conventional repellents are both available, applied by spray or immersion. They reduce the rate at which liquid soaks in, giving time to blot a spill.
Repellents wear with abrasion, so heavily used areas lose protection first, and re-application guidance belongs in the care instructions.
Stain-Resistant Treatment
Stain-resistant finishes slow the absorption of oils and dyes. They do not prevent staining from a spilled drink left in contact with the surface, and aggressive cleaning can strip the treatment.
Care Instructions
Care guidance for nap materials should state that brushing restores the surface, that water should be blotted rather than rubbed, that aggressive chemicals should be avoided, and that professional cleaning is preferable for significant staining.
Where a brand sells into markets with extended consumer protection expectations, guidance that includes what not to do is as important as what to do.
Treatment Options
| Treatment | Benefit | Limitation |
|---|---|---|
| Water repellent | Slows liquid absorption | Wears with abrasion |
| Stain resistant | Slows oil and dye uptake | Not permanent |
| Both combined | Broader protection | Higher cost, may alter hand feel |
| None | Lowest cost | Highest claim risk |
Quality Control for Suede and Nubuck
Inspection for nap materials focuses on surface condition, consistency and handling marks, which are usually caused before final assembly.
Appearance Checks
Inspectors look for uniform nap direction across assembled panels, absence of flattened or burnished areas, absence of adhesive marks and stains, and consistent colour under standard lighting. Panels should be inspected before assembly, because a defect hidden by assembly is the most expensive kind.
Physical Checks
Physical checks cover seam strength on reinforced panels, adhesion of bonded linings, and the behaviour of hardware attachments under load. A pull test on a handle attachment made from suede is more informative than the same test on grain leather, because the failure mode differs.
Common Defects
| Defect | Cause | Prevention |
|---|---|---|
| Nap direction mismatch | Uncontrolled cutting | Nap direction on pattern and instruction |
| Flattened patch | Heat or pressure during assembly | Protective pressing, reduced temperature |
| Adhesive mark | Strike-through | Viscosity control, thin application |
| Ragged edge | Dull blade | Blade change schedule |
| Stain or fingerprint | Handling | Gloves, covered work in progress |
| Edge paint wicking | Wrong edge finish | Folded or bound edge method |
| Seam slippage | Layer movement | Walking-foot machine, higher density |
Specifying Suede and Nubuck
Specifications for nap materials should remove interpretation, because many defects originate in assumptions rather than in workmanship.
Terminology and Source
State whether the material is suede, nubuck, sueded split or bonded suede, and specify the source layer. "Suede" alone leaves the supplier free to deliver a split-based material when nubuck was expected.
Nap Direction and Layout
Specify nap direction on the pattern, state the allowance for yield loss, and record the requirement in the cutting instruction. Where contrast is intentional, describe it explicitly and require a sample.
Sample Approval and Tolerance
Approve a sample in the production material and nap direction, and keep it as the reference for colour and surface. Nap materials vary between hides and between dye lots, so tolerances should be stated rather than assumed.
Specification Checklist
| Item | Must be specified |
|---|---|
| Material type and source layer | Yes |
| Nap direction | Yes |
| Colour reference sample | Yes |
| Yield allowance for nap | Yes |
| Reinforcement method | Yes |
| Edge finish method | Yes |
| Lining type and bonding | Yes |
| Treatment applied | Yes |
| Inspection criteria | Yes |
Cost Considerations
Nap materials change the cost structure in ways that a price comparison against grain leather does not reveal.
Material Yield
The nap direction constraint raises consumption, because patterns cannot be rotated freely around defects. In practice this means that two similar bags in suede and in grain leather may require materially different amounts of raw material.
Additional Processes
Reinforcement, lining, protective treatment and folded edge finishing are additional processes that grain leather bags may not require. Each adds labour and supervision.
Handling and Rework
Nap materials generate more handling defects, and a stain or flattened area cannot be repaired as easily as a scratch on finished grain. Rework rates are higher, and the losses are concentrated in the most expensive operation: assembly.
Cost Drivers
| Driver | Relative weight |
|---|---|
| Material consumption from nap constraint | Significant |
| Reinforcement and lining | Moderate |
| Protective treatment | Low to moderate |
| Edge finishing method | Moderate |
| Handling and rework | Moderate to high |
Common Misconceptions About Nap Leathers
Several beliefs lead buyers and factories into avoidable problems.
"Suede Is Simply a Cheaper Material"
Suede has its own cost structure, driven by yield constraints, additional processes and handling losses. A suede bag that uses adequate reinforcement is not automatically cheaper to produce than a smooth leather one.
"Nap Direction Is a Detail"
Nap direction determines whether assembled panels read as one material or as several. It belongs in the pattern, the cutting instruction and the inspection criteria, not in a comment about appearance.
"Nap Materials Cannot Carry Structure"
Suede and nubuck are used in structured bags regularly. The structure comes from reinforcement between the nap and the lining, which is a construction decision rather than a material limitation.
"Protective Treatment Makes the Material Waterproof"
Treatments slow absorption; they do not stop it. Expecting otherwise leads to claims when a spill is left in place, and to care instructions that contradict the product's actual behaviour.
Working With Nap Materials in Sampling
Sampling is where nap behaviour is either proven or discovered late, and the process should be adapted rather than copied from grain leather work.
Sample Quantity and Direction
Ask for at least two pieces in the first round: a full sample and a small panel set cut with the nap in the intended direction. The panel set lets you check tone and light response quickly, without dismantling a finished sample.
Where a design includes a deliberate contrast panel, request that version as a separate sample so the effect can be judged before the layout is locked.
Judging Colour Under Different Light
Nap materials shift in tone as the light source and viewing angle change. Judge samples under at least two lighting conditions, including daylight and the lighting typical of the sales channel, because a colour approved under one condition may look different in the other.
Photographs taken for internal approval should record the light source and angle, otherwise later comparisons become arguments rather than checks.
Keeping the Reference
Retain the approved sample, wrapped and stored away from light and dust, and use it for both production reference and later batches. Nap materials evolve with handling, so the reference should be handled as little as possible.
Sampling Practice
| Step | Purpose |
|---|---|
| Panel set with nap direction | Verify tone and direction |
| Full sample | Verify construction and hand feel |
| Contrast version | Judge intentional nap reversal |
| Two-light check | Confirm colour under both conditions |
| Reference storage | Protect the approved standard |
Nap Materials by Bag Category
The suitability of suede and nubuck varies by bag type, and the construction adjustments follow the use pattern.
Small Leather Goods and Pouches
Nap materials work well in small items, where loads are light and panels are small. The main risks are staining from frequent handling and edge finishing on curved shapes, both managed through folded edges and treatment.
Shoulder and Crossbody Bags
These carry moderate loads and contact the body, so reinforcement at strap attachments and resistance to perspiration staining matter. Nubuck generally performs better than suede in this category because it holds shape and resists stretching.
Totes and Larger Bags
Large panels of split-based suede can distort under weight unless the construction includes reinforcement and a bonded lining. Where the design calls for a soft, unstructured shape, the load should be limited by design rather than by reinforcement alone.
Structured and Formal Bags
Nubuck can be used in structured designs when the reinforcement is placed between the nap and the lining and the edges are folded. The result is a structured bag with a softer surface than a grain leather equivalent.
Category Guidance
| Category | Suitable material | Key construction point |
|---|---|---|
| Small pouches | Suede or nubuck | Folded edges, treatment |
| Crossbody | Nubuck preferred | Reinforced attachment points |
| Tote | Nubuck, or reinforced suede | Bonded lining, base support |
| Structured bag | Nubuck | Internal reinforcement, folded edges |
| Lined interior | Both | Bonded or stitched to reinforcement |
Packaging, Storage and Retail Handling
Nap materials can be marked after the bag is finished and inspected, which makes packing a production step rather than a formality.
Packaging Materials
Use wrapping that does not shed fibres or transfer ink. Tissue paper marketed as colour-fast and unprinted is safer than recycled paper with visible printing, because ink can transfer to the nap under pressure.
Dust bags should be made from a smooth, lint-free material. Coarse fabric can abrade the nap during transport.
Storage and Stacking
Nap surfaces should not be stacked face to face under weight, because pressure flattens the fibres and can leave permanent marks. Bags stored for a season should be filled lightly to hold shape, wrapped individually, and stored without direct weight on the nap face.
Humidity should be controlled rather than eliminated; extremely dry storage can make the nap brittle, while damp storage encourages staining and mould.
Retail Handling
Retail handling marks are a common source of returns for nap materials, because staff and customers touch the surface while browsing. Providing gloves for staff who handle the products, and positioning the bags where they are lifted rather than dragged, reduces the issue.
Care cards should state plainly that nap materials change with brushing and handling, which sets expectations before purchase rather than after.
Handling Through the Supply Chain
| Stage | Risk | Control |
|---|---|---|
| Packing | Ink transfer, fibre shedding | Unprinted colour-fast wrap |
| Dust bag | Abrasion in transit | Smooth lint-free fabric |
| Storage | Pressure marks | Individual wrap, no stacking load |
| Humidity | Staining, mould or brittleness | Controlled storage conditions |
| Retail display | Handling marks | Gloves, lifting practice |
| Customer communication | Misread tonal change | Care card explaining nap behaviour |
Sourcing Nap Materials From Suppliers
Nap materials vary between hides and between dye lots, and the questions asked at sourcing stage determine how much of that variation reaches the customer.
Questions That Predict Behaviour
Ask whether the material is suede, nubuck or a sueded split, and from which layer. Ask how the nap is produced, whether the hide was buffed before or after dyeing, and whether the supplier recommends the material for folded edges.
Ask also about reinforcement recommendations. A supplier who understands where the material stretches can advise which panels need backing, which saves a sampling round.
Batch Consistency and Inspection
Nap materials vary in nap height, tone and handle between lots. Ask for a colour reference for each lot, and inspect incoming material against the approved standard before cutting begins.
Where several lots will be used in one run, cut panels from a single lot for each bag wherever possible, and keep the lots separated on the floor so a mixed assembly cannot happen by accident.
Documentation Worth Keeping
Record the lot reference for each production batch, the treatment applied, and the supplier's care guidance. This information supports any later claim, and it makes a repeat order reproducible rather than approximate.
Supplier Questions
| Question | Why it matters |
|---|---|
| Suede, nubuck or sueded split? | Determines strength and behaviour |
| Which layer is used? | Predicts stretch and durability |
| Buffed before or after dyeing? | Affects colour depth and nap |
| Suitable for folded edges? | Determines edge method |
| Reinforcement advice? | Reduces sampling rounds |
| Lot colour reference? | Enables incoming inspection |
| Recommended treatment? | Aligns finish with material |
FAQ
What is the difference between suede and nubuck?
A: Suede is buffed on the flesh side, often from a split layer, giving a soft short nap. Nubuck is buffed lightly on the grain side of a full-grain hide, so the strong grain layer remains intact and the material holds shape better.
Why does nap direction matter so much?
A: Brushing with or against the nap produces lighter or darker tones. If panels are cut in mixed directions, the assembled bag shows visible tonal blocks that no finishing can remove.
Does nap direction increase material consumption?
A: Yes. Cutting all pieces in one direction removes the freedom to rotate patterns around defects, which typically raises consumption compared with a material where orientation does not matter.
Can suede bags be lined?
A: They are usually lined. A lining stabilises the panel, prevents the nap interior from collecting debris and reduces stretching. Bonding the lining to the panel is common where the bag carries weight.
How should suede edges be finished?
A: Folded or bound edges usually replace edge paint, which wicks into the nap and produces a dark, uneven line. The panel edge must be skived accurately for a folded finish to sit flat.
Will a protective treatment make suede waterproof?
A: No. Water-repellent treatments slow absorption so a spill can be blotted, but they do not prevent liquid from soaking in if it is left in contact with the surface.
What causes flattened patches on suede panels?
A: Heat and pressure. Pressing at high temperature, stacking bags face to face or applying localised weight can crush the nap permanently, which is why pressing should use the lowest effective temperature and a protective cloth.
Is nubuck stronger than suede?
A: Generally yes. Nubuck is built on the grain layer, which resists stretching, while suede is often made from a split with lower tensile strength. Reinforcement remains advisable in load-bearing areas for both.
How do I inspect suede or nubuck bags in production?
A: Check nap direction consistency across panels, absence of flattened or burnished areas, no adhesive or handling marks, and colour consistency under standard lighting. Panel-level inspection before assembly catches most defects.
Why does my suede bag look different from the photograph?
A: Nap surfaces shift in tone depending on light angle and brushing direction. This is inherent to the material, which is why approval should happen under at least two lighting conditions.
Can bonded suede be used instead of natural suede?
A: Bonded suede is a reconstituted material with lower strength and different behaviour in folding, pressing and edge finishing. It suits light decorative uses rather than load-bearing panels.
How should a suede bag be cleaned?
A: Brushing restores the nap, spills should be blotted rather than rubbed, and aggressive chemicals should be avoided. Significant staining is best handled professionally, and instructions should say so.
Do suede and nubuck bags need reinforcement for hardware?
A: Yes. Hardware attachment points concentrate load, and a nap material can stretch or tear at those points. A backing patch or reinforcement layer behind the attachment is standard practice.
Why do stitches disappear on suede?
A: Thread sinks into the nap, so a stitch line that reads clearly on grain leather may be almost invisible. Where a visible stitch is part of the design, it must be approved on a sample rather than assumed.
How should finished suede bags be packed?
A: Wrap in unprinted, colour-fast material, avoid stacking with weight on the nap face, and use a smooth lint-free dust bag. Ink transfer and pressure marks happen after inspection, not during production.
Is suede cheaper to produce than smooth leather?
A: Not necessarily. Nap constraints raise material consumption, and reinforcement, lining, edge finishing and treatment add processes. The comparison depends on the construction, not on the surface alone.
Ready to build a suede or nubuck bag that survives real use? Share your design, intended market and the nap material you are considering, and we will help you specify what actually determines the outcome: consistent nap direction, reinforcement where load is carried, edge and lining methods that suit a nap surface, and treatment plus care guidance that match what the material can realistically deliver.